
Case Studies
For operations across the United States, effective dust management is critical to protecting workers, maintaining compliance, and improving site performance. Mideco’s case studies showcase how our proven dust control solutions are being applied in real-world environments, from mining and quarrying to grain handling, processing plants, and bulk material transfer facilities.
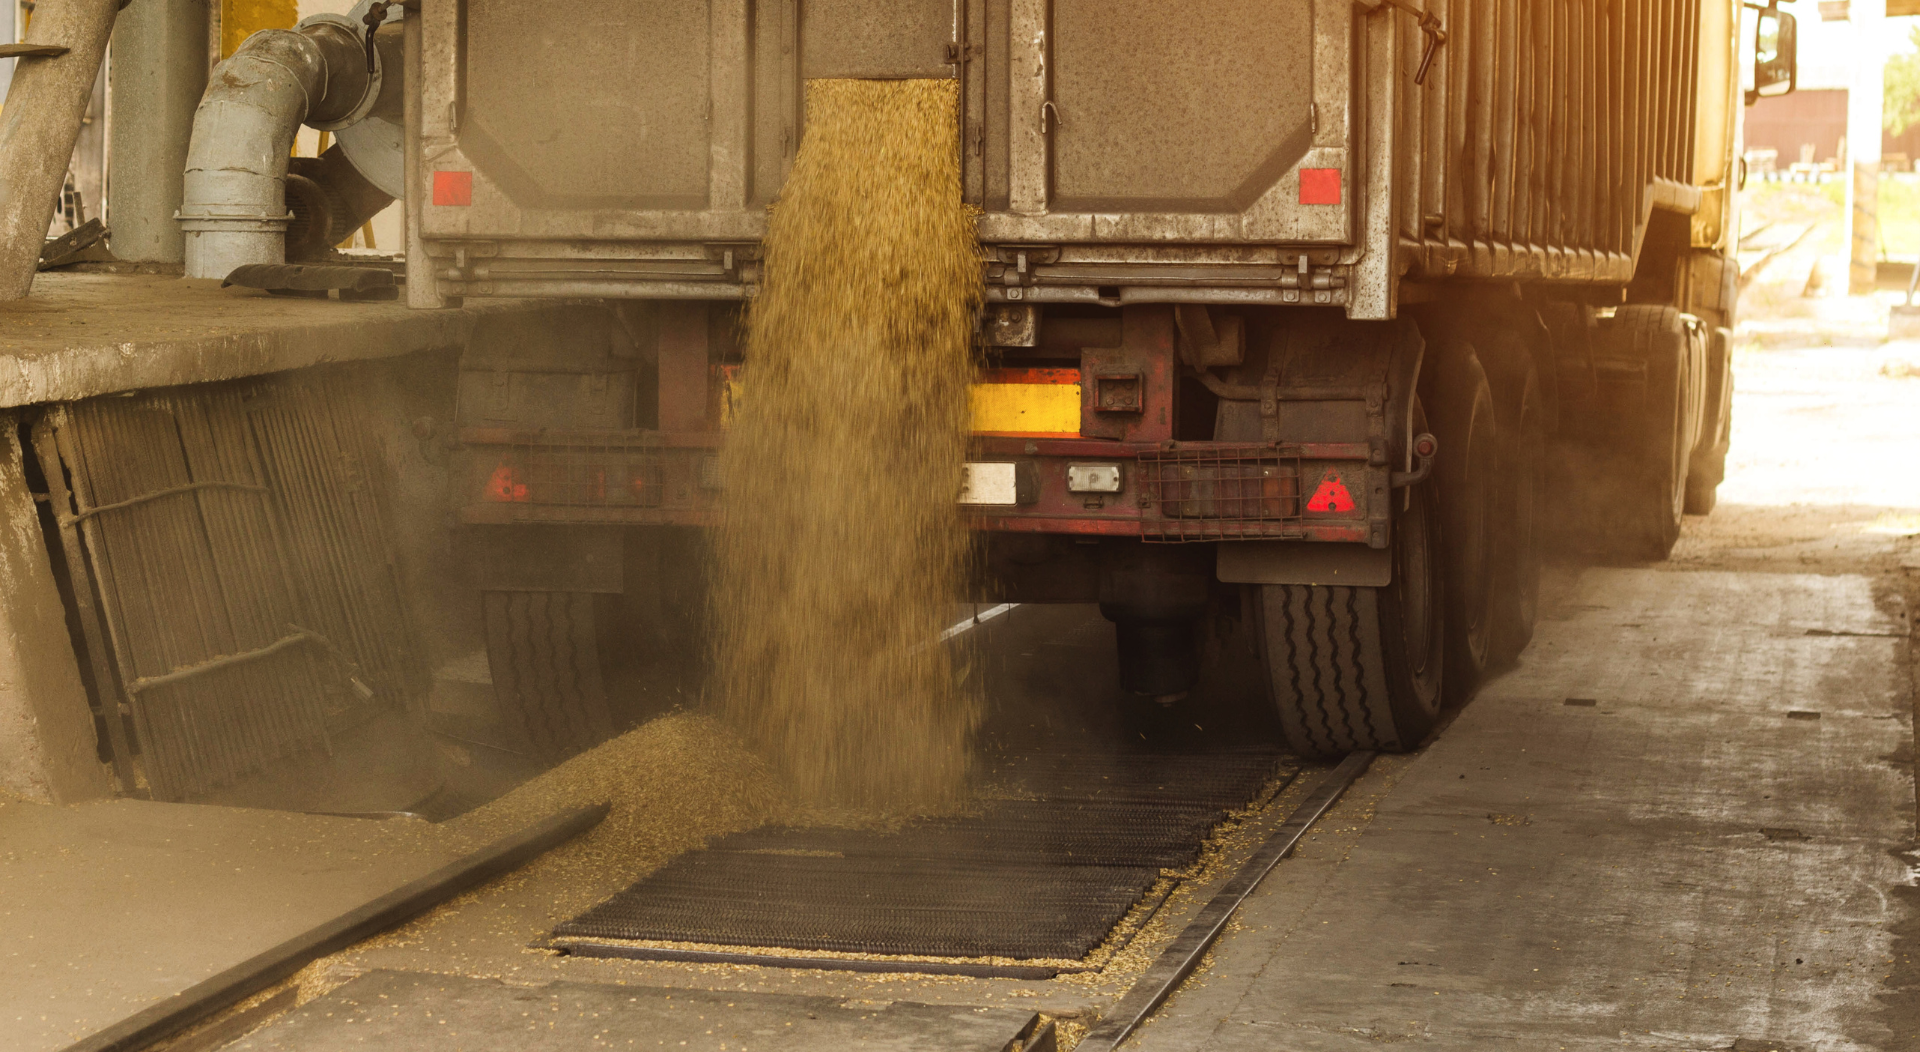
Our internationally patented Burnley® Baffles are installed in receiving pits and dump hoppers to deliver effective dust suppression by controlling airflow and reducing airborne dust emissions. For personnel protection, the Bat Booth® provides fast and reliable dust extraction from workers’ clothing and PPE in just seconds, helping reduce secondary dust exposure and contamination across site facilities. Supporting enclosed workspaces, the Bat Vent® delivers filtered, pressurized clean air to control rooms, offices, and break rooms located near dust-generating operations.
Together, these systems form part of a complete industrial dust collection system strategy designed to improve air quality, reduce fugitive dust, and support safer operations. Our US case studies highlight how Mideco’s dust extraction systems continue to help industrial sites achieve cleaner, safer, and more efficient working environments through practical, engineered dust control solutions.
Real-world results that speak for themselves

Burnley® Baffles – Groff Julius
Delaware, USA 2023
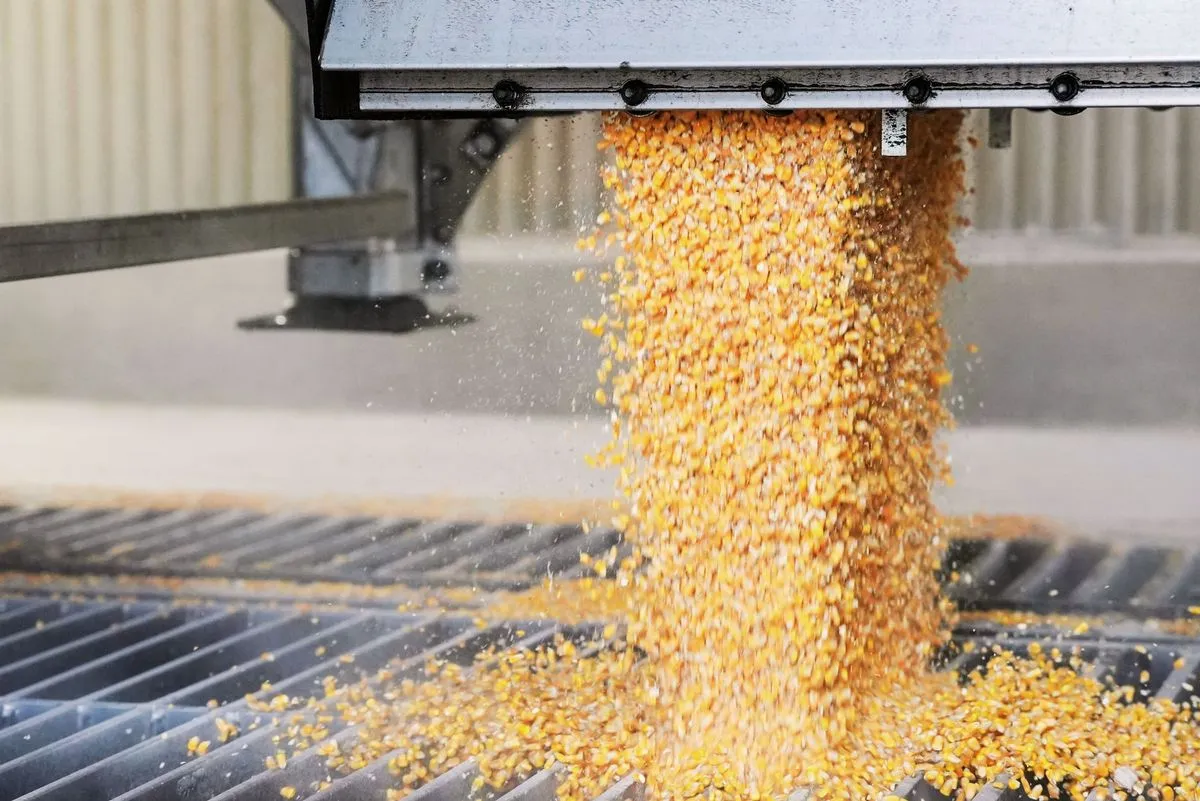
Burnley® Baffles – AMG, Inc. for Primient
Tennessee, USA 2023

Burnley® Baffles – Arrow Commodities
Australia, 2023

Burnley® Baffles – WL Port-Land Systems Inc for Mountaire Farms, USA 2022
Maryland, USA 2022

Bat Vent® 1.0 – Holcim Oaklands Junction Concrete
Australia, 2021

Bat Booth® – 3M IMPD Pittsboro Plant
North Carolina, USA 2020

Bat Booth® – John Deere Waterloo Works
Iowa, USA 2019

Bat Booth® – Heidelberg Materials
Australia 2019

Burnley® Baffles and ECP Dust Collectors – Ahrens
Australia 2019

Bat Booth® – Bis Industries
Australia 2019

Bat Booth® – BHP Olympic Dam
Australia 2017

Burnley® Baffles and ECP Dust Collectors – Qube Ports
Australia 2014
Take the lead in workplace safety.
Fill in the form for a quote or consultation on OSHA-compliant dust management solutions for your facility.
"*" indicates required fields

Mideco Jia Pty Ltd
Global leader in Dust Management Solutions since 1950. Supporting North American grain operations with industry-standard technology for over 40 years.Helper Links
Trusted by Industry Leaders

Copyright 2026 © Mideco
