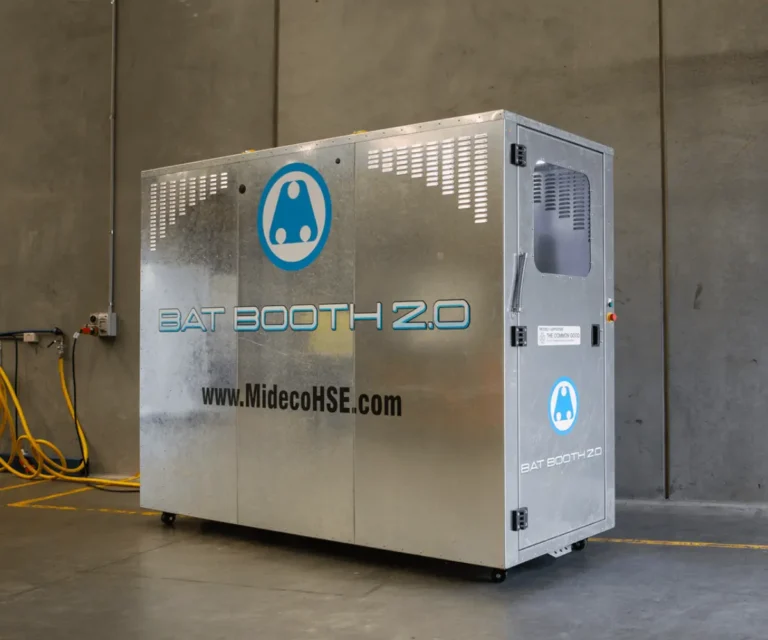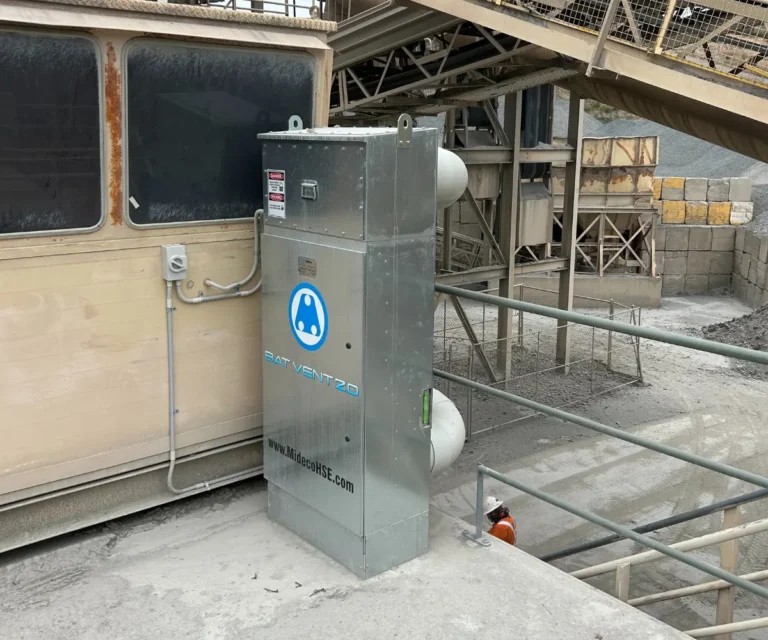
Branded products
Dust control solutions
Home » Industries »
Precision, purity and compliance are non-negotiable in pharmaceutical manufacturing. Whether you’re producing tablets, capsules or powders, even the smallest dust particles can impact worker safety, product quality and regulatory compliance.
Mideco provides high-performance pharmaceutical dust collection systems engineered for the controlled environments of drug production. Our specially engineered solutions maintain air quality, protect staff and keep your business inline with the strict standards that govern the pharmaceutical industry.
Our solutions can also be found in other sectors that require industry-specific industrial dust extraction solutions, including dust collection solutions in Mines, dust collection in Bulk Material Handling, and dust collection solutions in Quarries.
Watch videoCompressing and coating tablets generates fine airborne particles—particularly when APIs are involved.
Mixing powdered raw materials creates airborne dust that can quickly travel across cleanroom zones without proper extraction.
Filling capsules or containers at high speeds can cause small but consistent dust dispersion.
Manual or semi-automated handling of powders is a key area for worker exposure and product loss—similarly to environments like dust collection solutions in Farms where fine airborne particles pose health and product safety concerns.
Enquire nowIn pharmaceutical environments, dust stems from nearly every stage of production—particularly when working with active pharmaceutical ingredients (APIs) and fine powders. Without effective dust collectors for pharmaceutical applications, facilities face multiple risks:
Managing pharmaceutical dust collection requires high-performance systems capable of containing fine particles. The key challenges include:
Health risks: Handling hazardous or potent materials that require full containment and operator protection
Potential contamination: Preventing cross-contamination between drug batches and cleanroom zones
Industry-specific compliance: Meeting global compliance standards such as FDA, GMP and OSHA guidelines
Maximising airflow: Capturing sub-micron dust particles without compromising airflow or cleanroom integrity
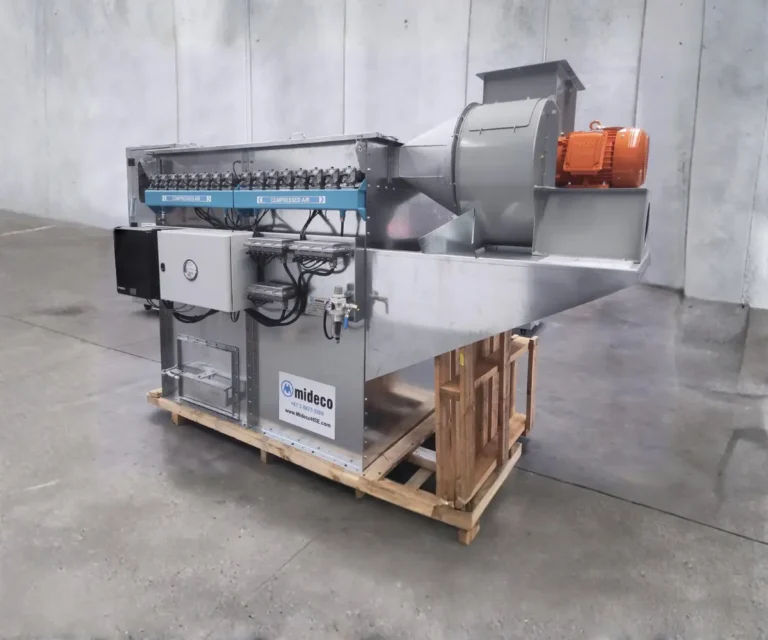
At Mideco, our range of dust collectors for pharmaceutical production environments is comprehensive, combining cleanroom compatibility with exceptional filtration efficiency.
Select filters that meet pharmaceutical standards, including HEPA or ULPA for fine particulate removal.
Use source capture for high-risk tasks such as weighing or blending, to contain dust before it spreads.
Implement regular maintenance and performance checks to avoid downtime and maintain cleanroom compliance.
With over 70 years of experience, Mideco is a trusted provider of high-performance pharmaceutical dust collection systems. Our solutions help clients meet regulatory standards, protect workers, maintain product quality and improve air quality. Whether you’re in pharmaceuticals, quarrying or mining, our specialist systems are engineered to perform in high-risk, regulated environments across the globe.
Mideco’s proven pharmaceutical dust collection systems are built to support the demands of modern pharmaceutical production—from research labs to full-scale operations.
Contact us today to discuss a custom industrial dust extraction solution, and safeguard your workers and workplace from bad quality air today.
Ready to elevate your workplace?
Contact Mideco for innovative dust management solutions.
"*" indicates required fields