Branded products
Dust control solutions
Home » Industries »
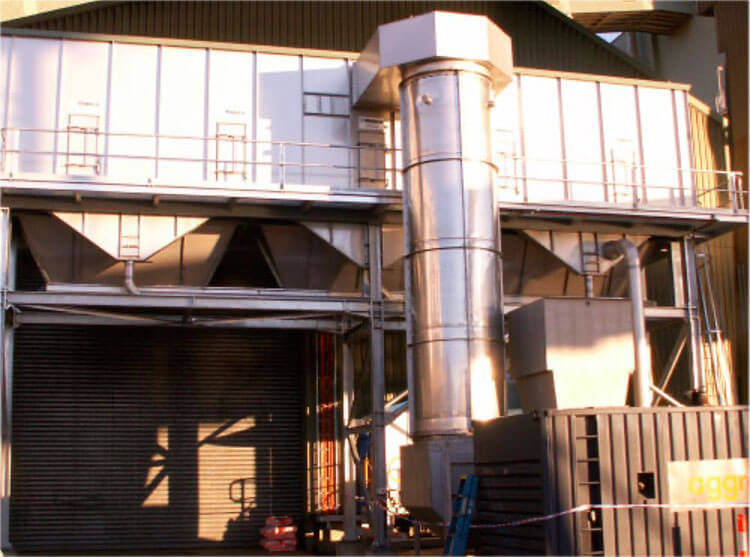
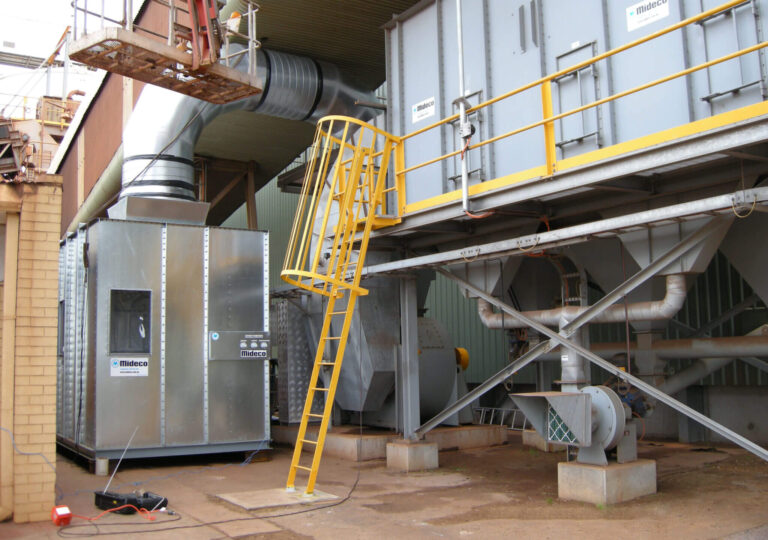
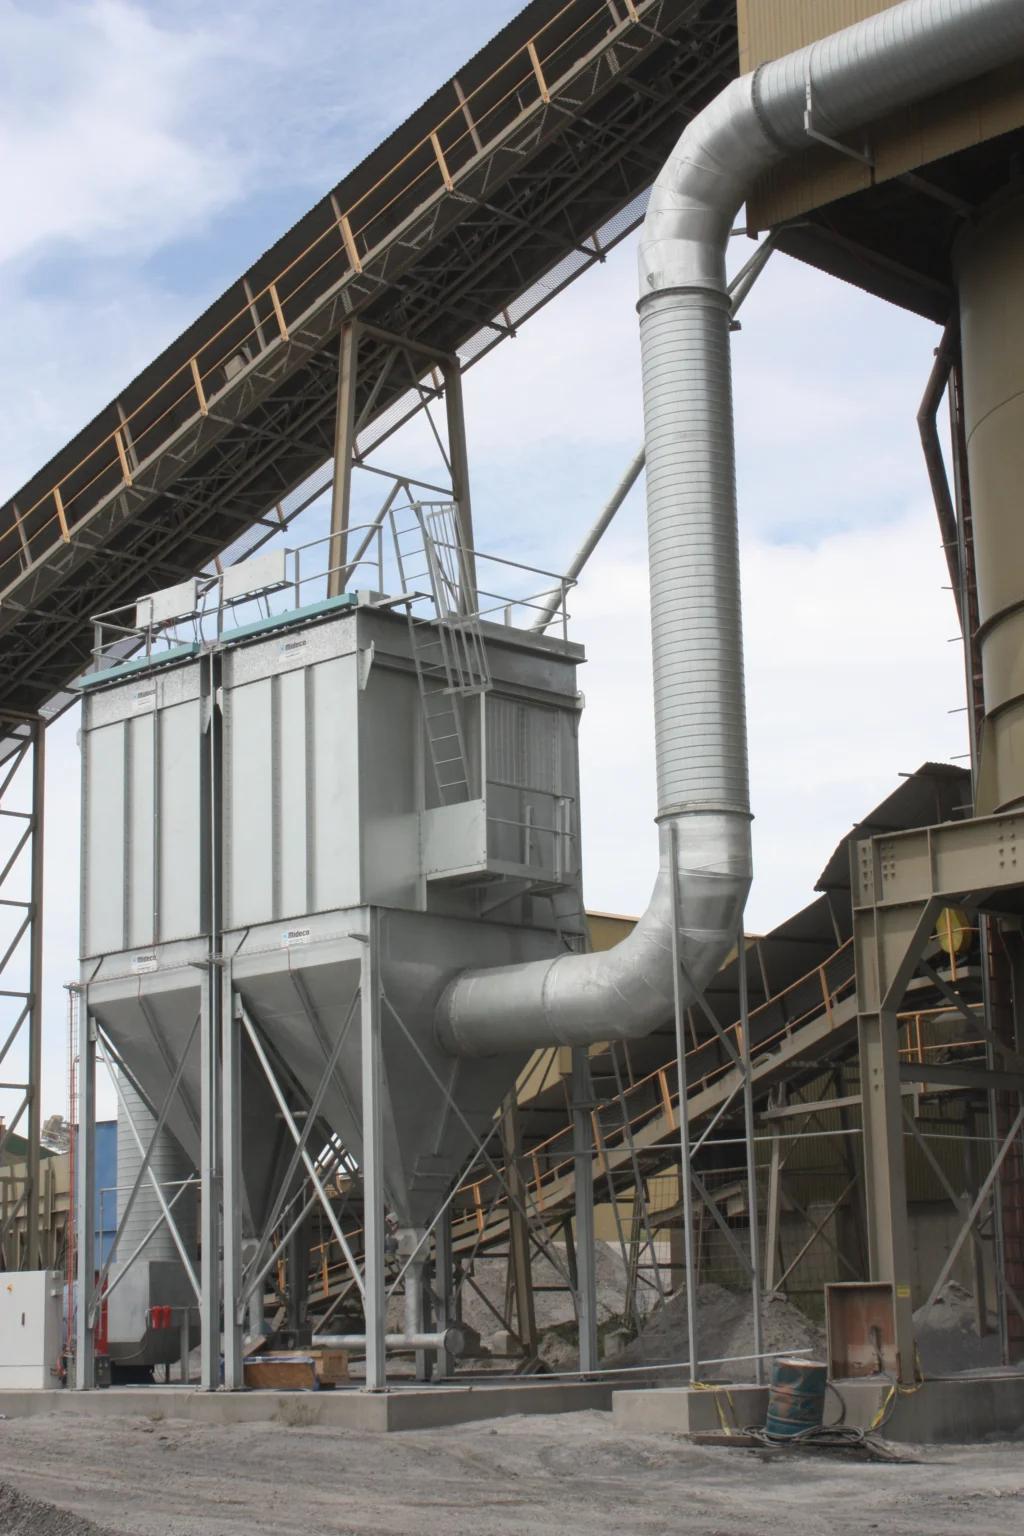
Dust is an unavoidable by-product of your mining operations, but left unmanaged, it becomes a serious health, safety and compliance issue. Mideco specialises in dust collection systems engineered to tackle the industry-specific challenges of dust control in mining, helping to protect your people, equipment and environmental performance.
Whether it’s above ground or deep underground, our highly experienced team understands the complexity of dust in mining environments, allowing us to deliver reliable, custom solutions that safeguard your business long into the future.
We also support other high-risk industries with a range of effective solutions: dust collection in bulk material handling, dust collection solutions in quarries, and dust collection in pharmaceuticals.
Watch videoCrushing and screening processes produce large volumes of fine dust particles. Without adequate capture, this dust spreads quickly and poses serious inhalation risks.
Material transfer between conveyor systems creates friction, spillage and turbulence—common causes of fugitive dust.
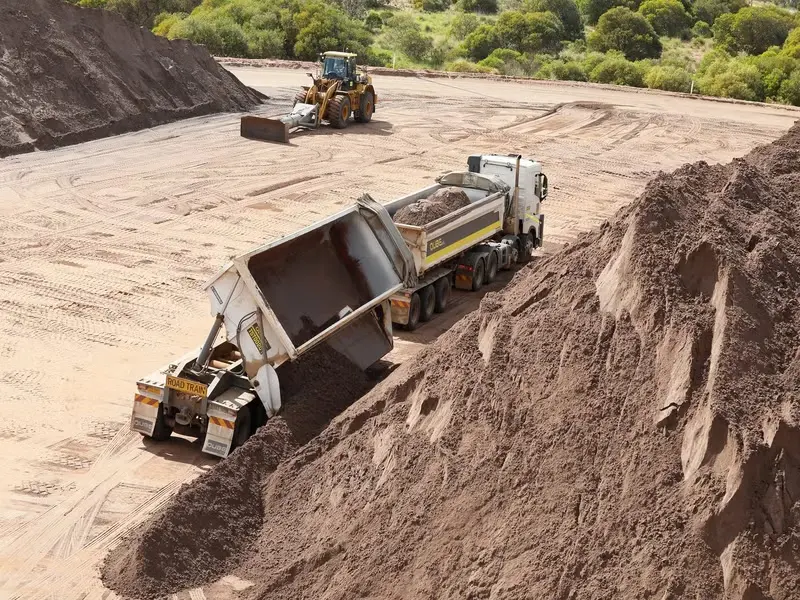
Mechanical disturbance and wind erosion around open stockpiles and loading areas may lead to widespread dust emissions.
Ventilation is often limited in underground settings, intensifying dust exposure and requiring highly efficient industrial dust extraction systems to maintain air quality.
Enquire nowMining dust isn’t just a nuisance—it’s abrasive, persistent and potentially dangerous. Getting on top of dust control in the mining industry means addressing several key challenges:
Health risks: Prolonged exposure to respirable crystalline silica and other particles can lead to serious respiratory illnesses, including silicosis.
Equipment wear: The abrasive nature of dust causes excessive wear and tear on machinery, increasing maintenance costs and reducing service life.
Regulatory compliance: Stringent environmental and workplace health standards demand proactive and reliable dust control systems.
Cost-efficiency: As with all aspects of the mining industry, balancing effective dust suppression with operating costs requires smart design and foresight.
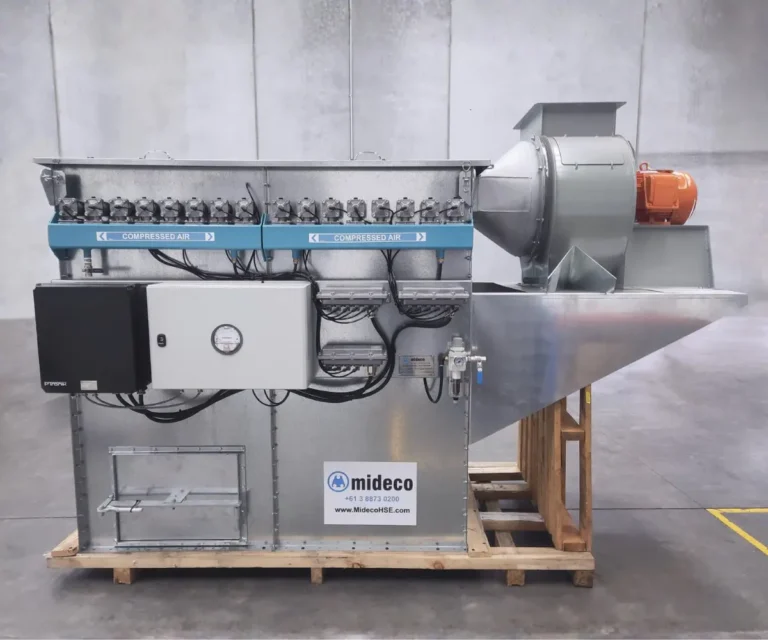
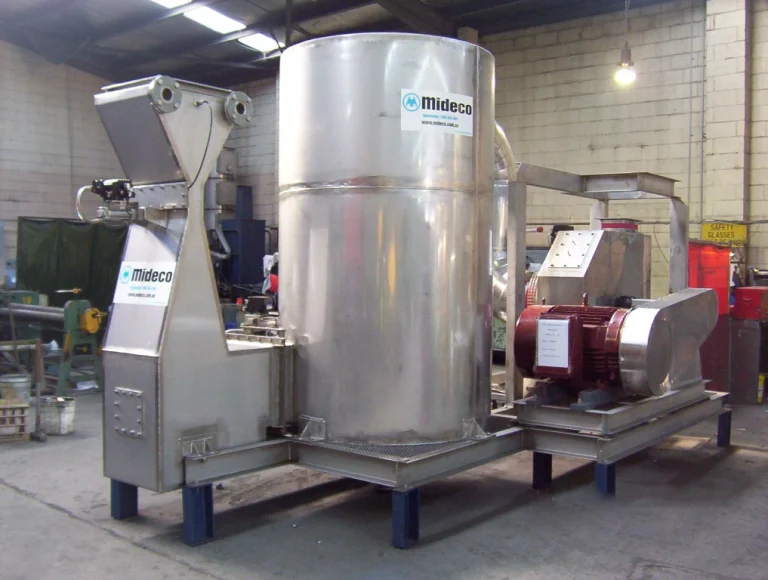
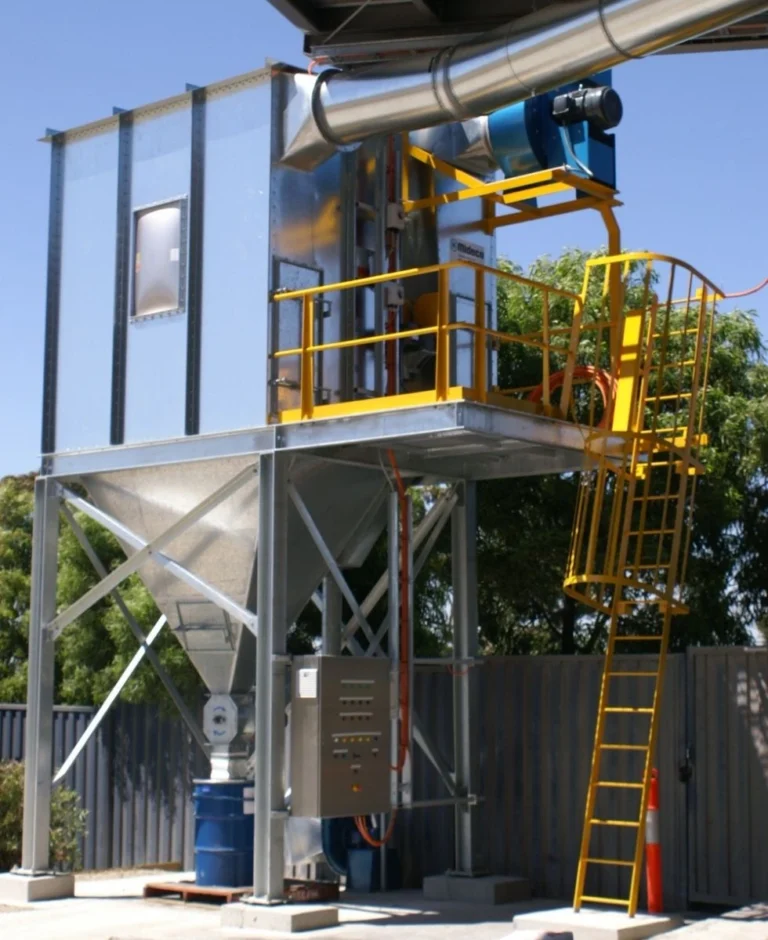
At Mideco, you can discover a range of dust collection systems engineered specifically for mining environments. Our approach fuses high-performance hardware with technical expertise, allowing for long-term control, minimal downtime and regulatory compliance.
It doesn’t matter if you’re looking for dust collection solutions in Farms or mine, open-air environments or closed, getting the most out of your dust collection system all comes down to smart design and ongoing care. Some of the key best practices include:
Positioning collectors close to dust sources to maximise capture efficiency and reduce the spread of airborne dust.
Choose the right filter media to match dust characteristics, including particle size, moisture content and level of abrasiveness.
Stick to a maintenance schedule, with routine checks and servicing to help maintain performance and prevent costly downtime.
Using leak detection tools such as fluorescent dye powder and pressure gauges help identify issues early before the damage is caused.
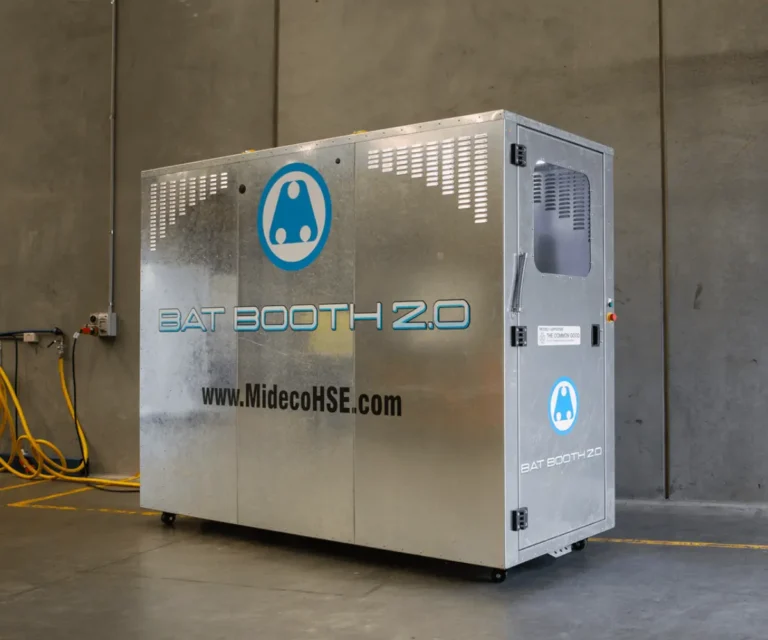
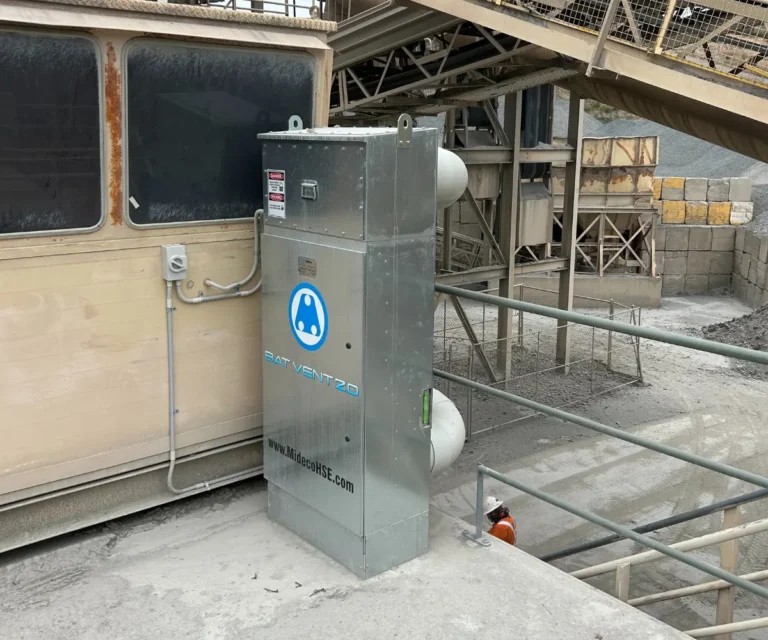
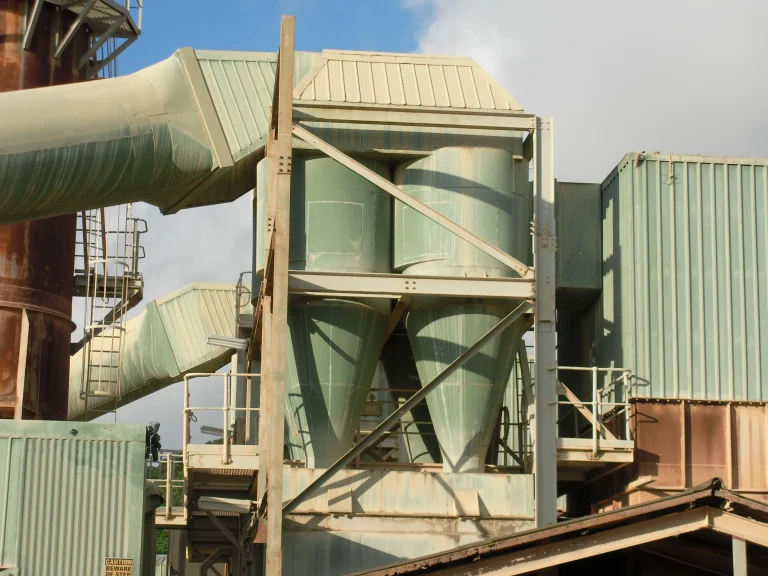
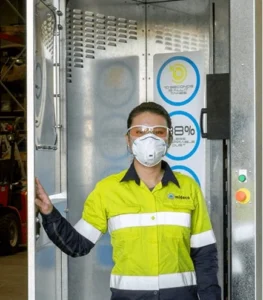
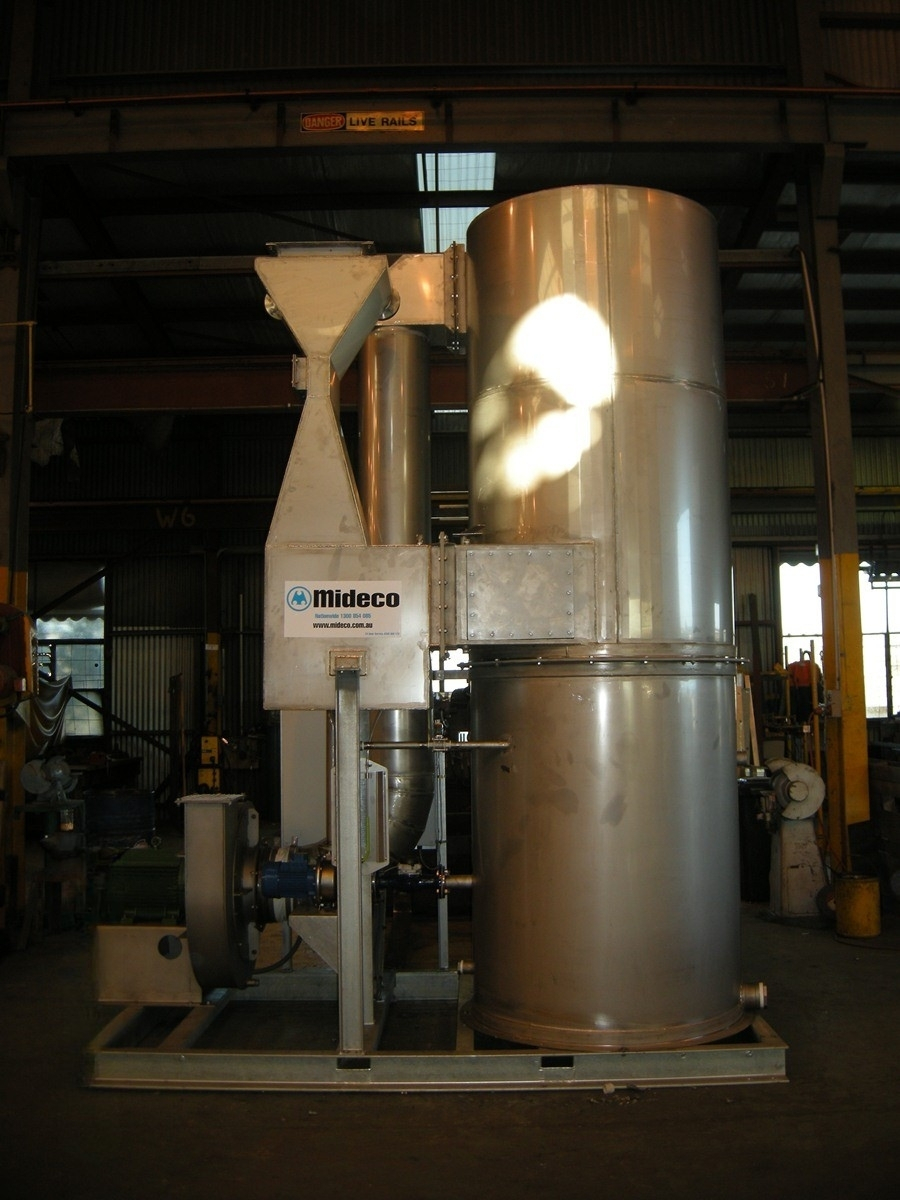
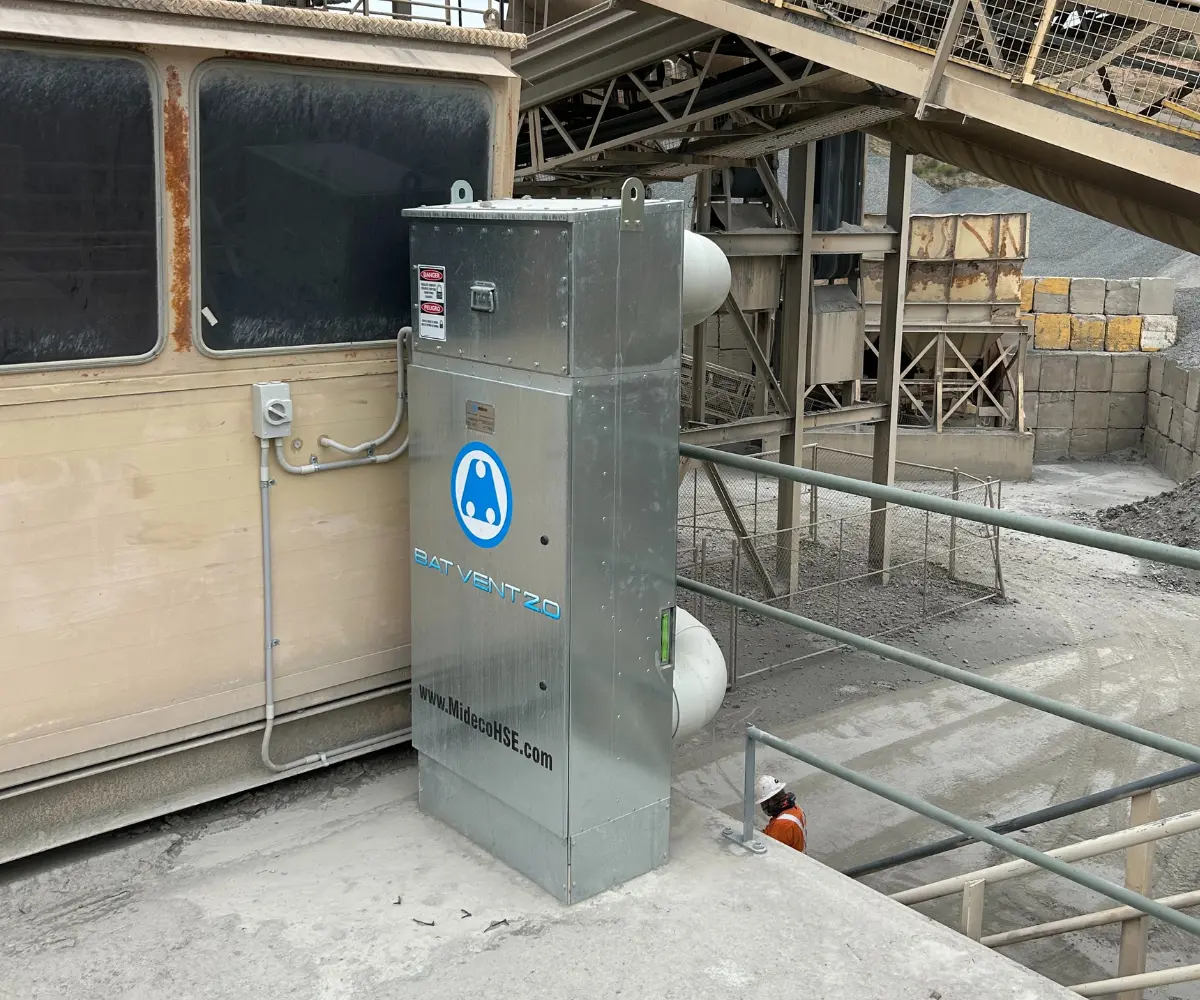
For over 70 years, Mideco has supported mining operations across Australia and globally with dust collection systems built for tough conditions. We deliver custom-designed extraction systems, advanced filtration technologies like Burnley® Baffles and Mideclone cyclones, and the Bat Booth®—our patented clothes dedusting unit.
From large operators to emerging ventures, we work alongside you to design and build solutions that perform in the harshest mining environments.
Reduce airborne contaminants, extend equipment life and meet occupational health and safety standards with our help.
Don’t wait for your duster control problem to impact your mine—contact Mideco and maximise your air quality today.
Ready to elevate your workplace?
Contact Mideco for innovative dust management solutions.
"*" indicates required fields