Branded products
Dust control solutions
Mechanical Dust Suppression for Bulk Material Transfer
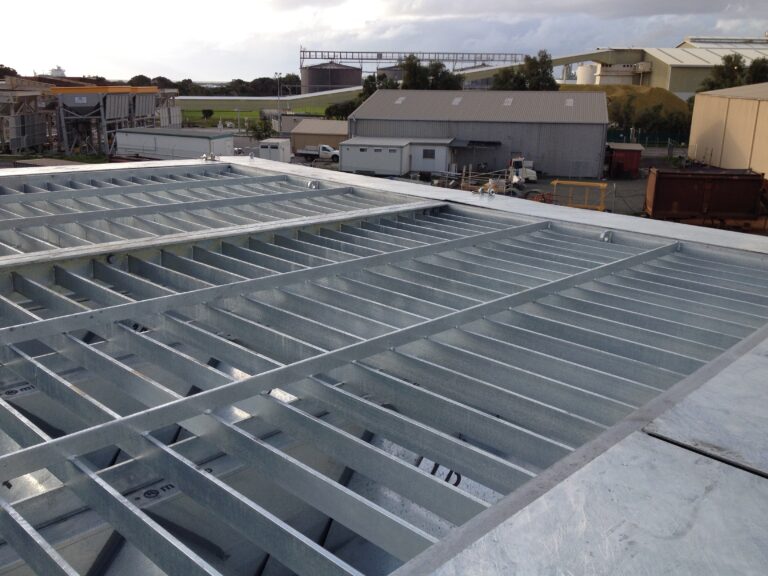
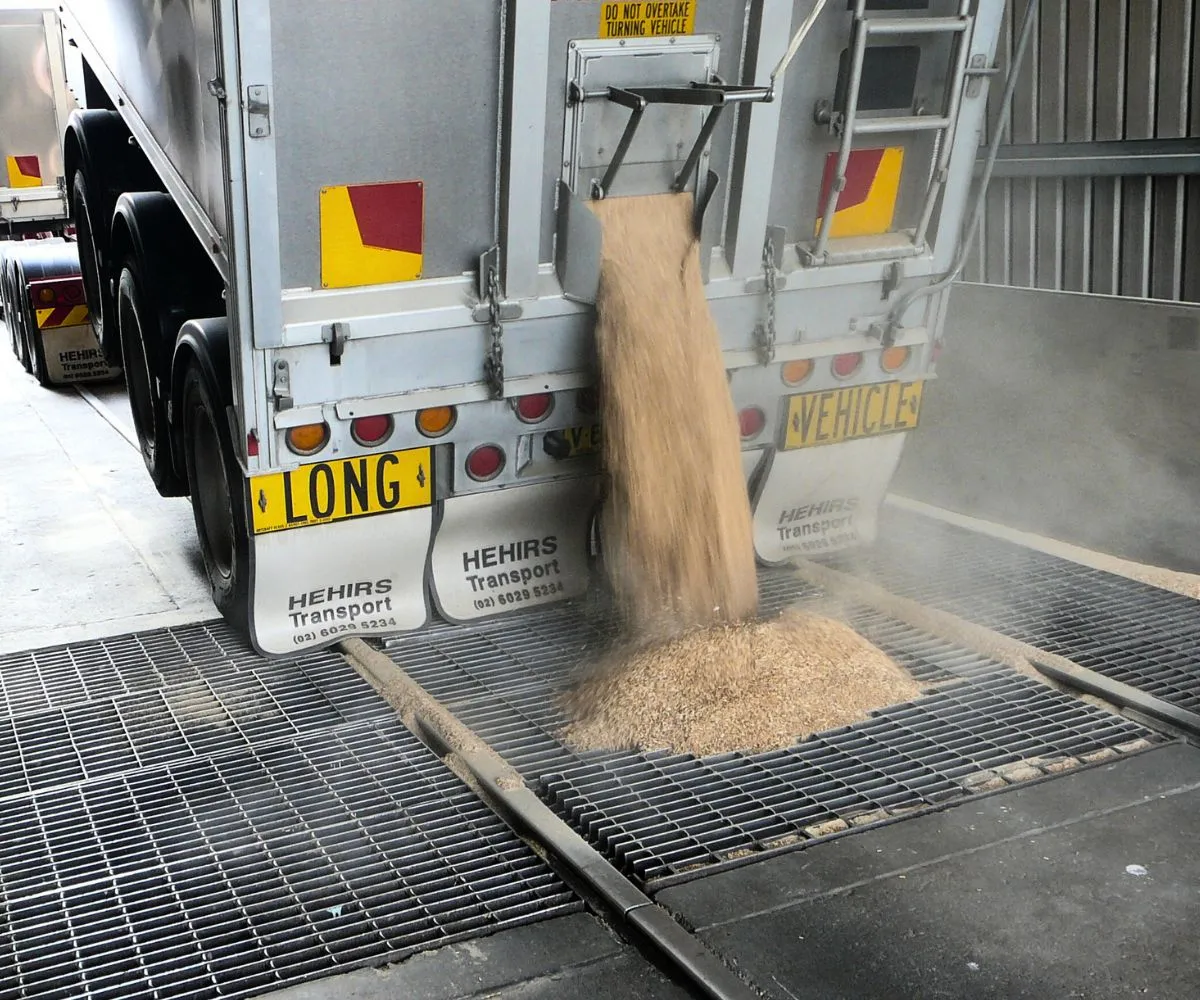
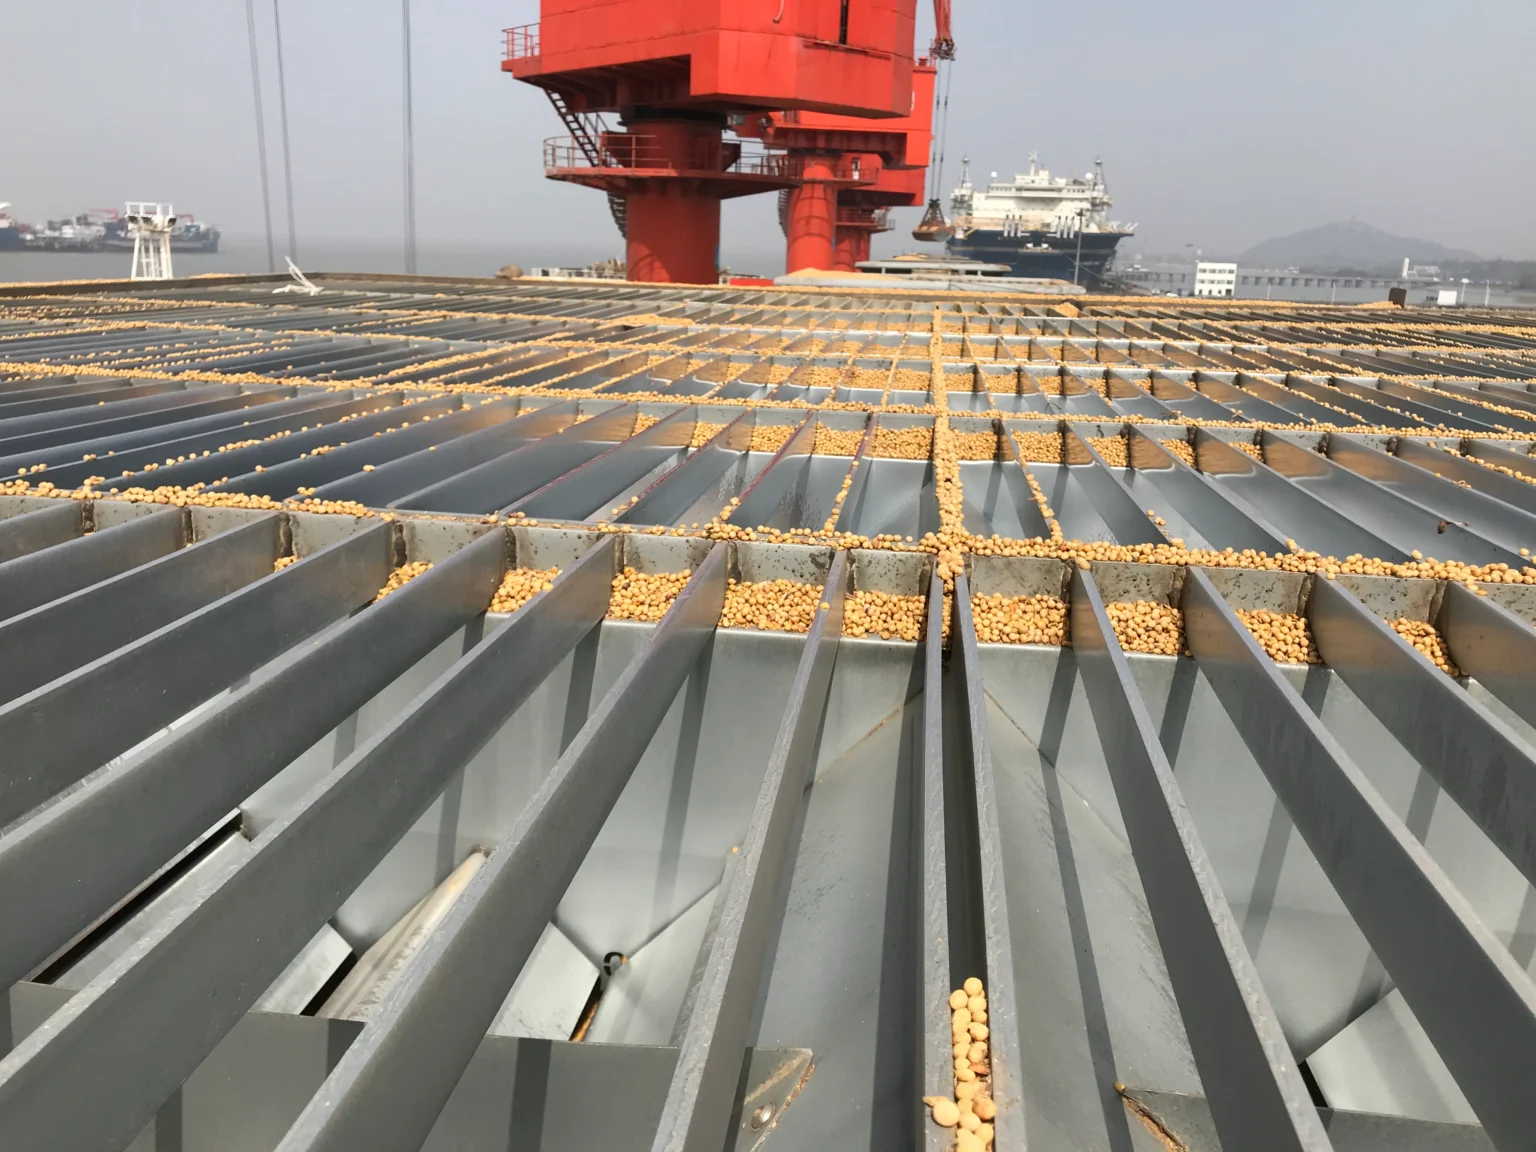
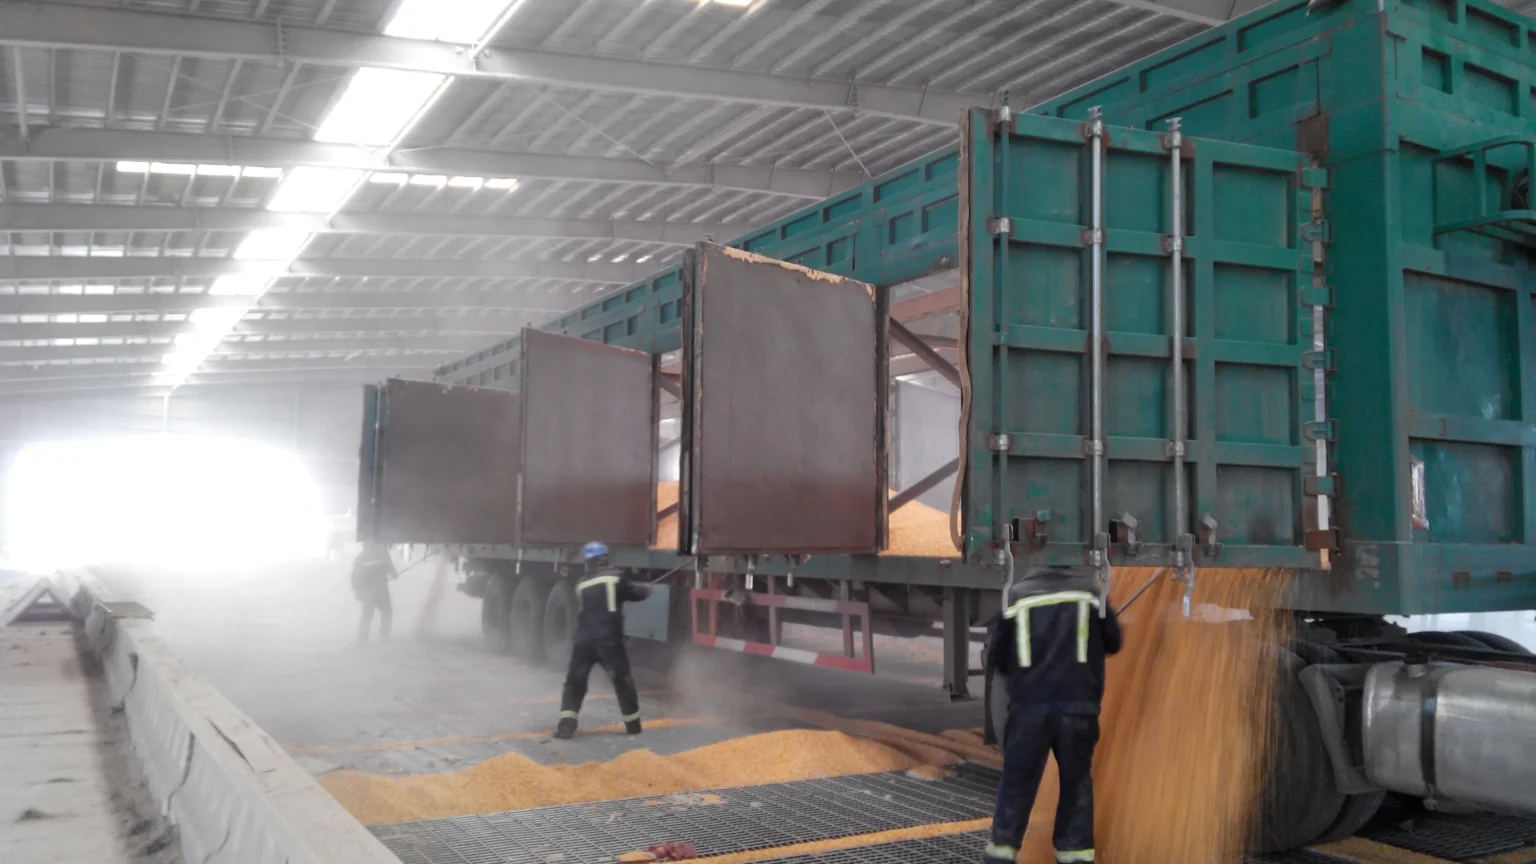
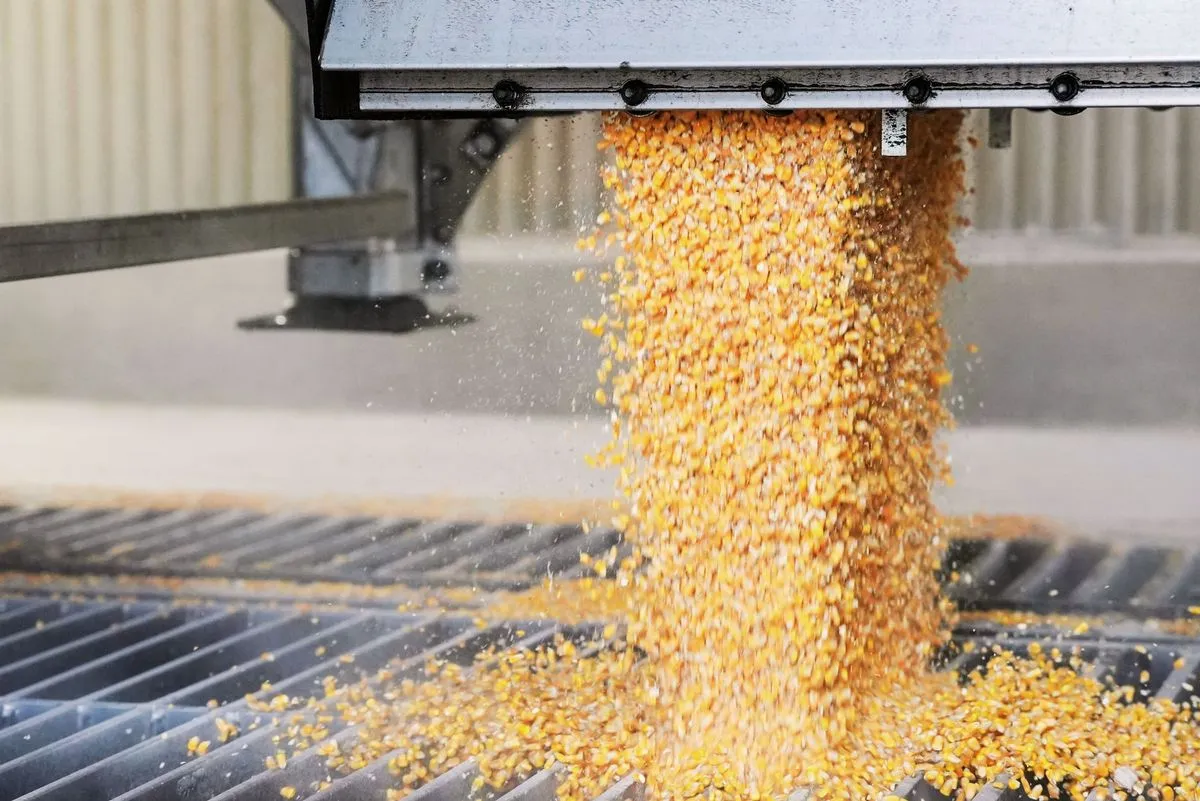
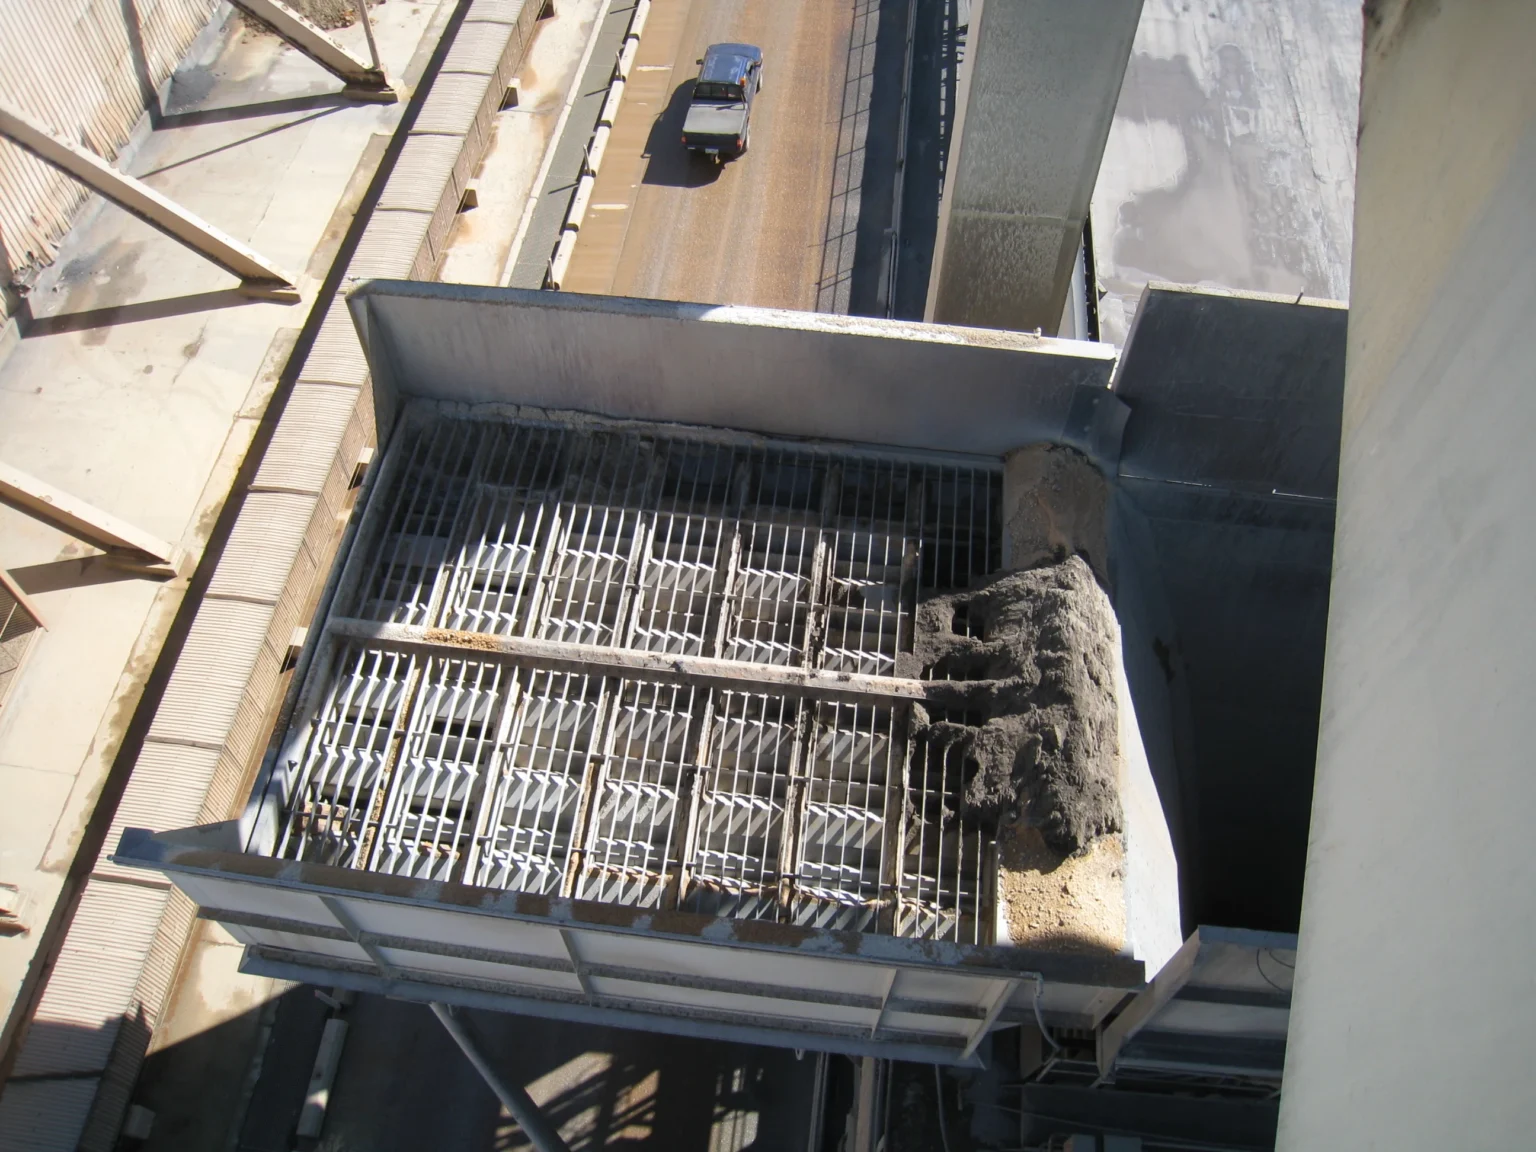
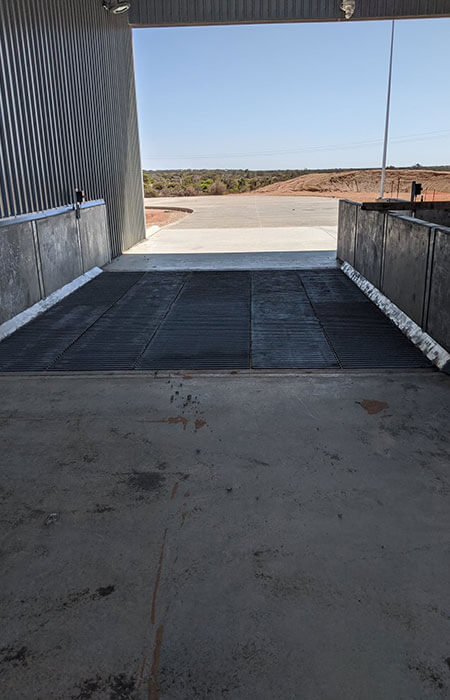
Burnley® Baffles control fugitive dust at dump hoppers and receiving pits where dry bulk materials create intense upward air displacement. During unloading, when the material hits the hopper, displaced air escapes through the falling product stream, carrying fine dust and light valuable material into the atmosphere.
Burnley Baffles regulate this airflow mechanically. A series of gravity-operated baffles fills the hopper inlet, creating uniform resistance across the surface. This slows and equalises air velocity, preventing high-speed air from carrying particles upward. The system suppresses up to 80% of dust when installed alone. When paired with a dust collector beneath the hopper, it achieves complete dust control.
Mining, quarrying, cement, grain, fertiliser, port, and ore handling operations rely on Burnley® Baffles to reduce airborne exposure, improve site safety, and limit product loss during material transfer.
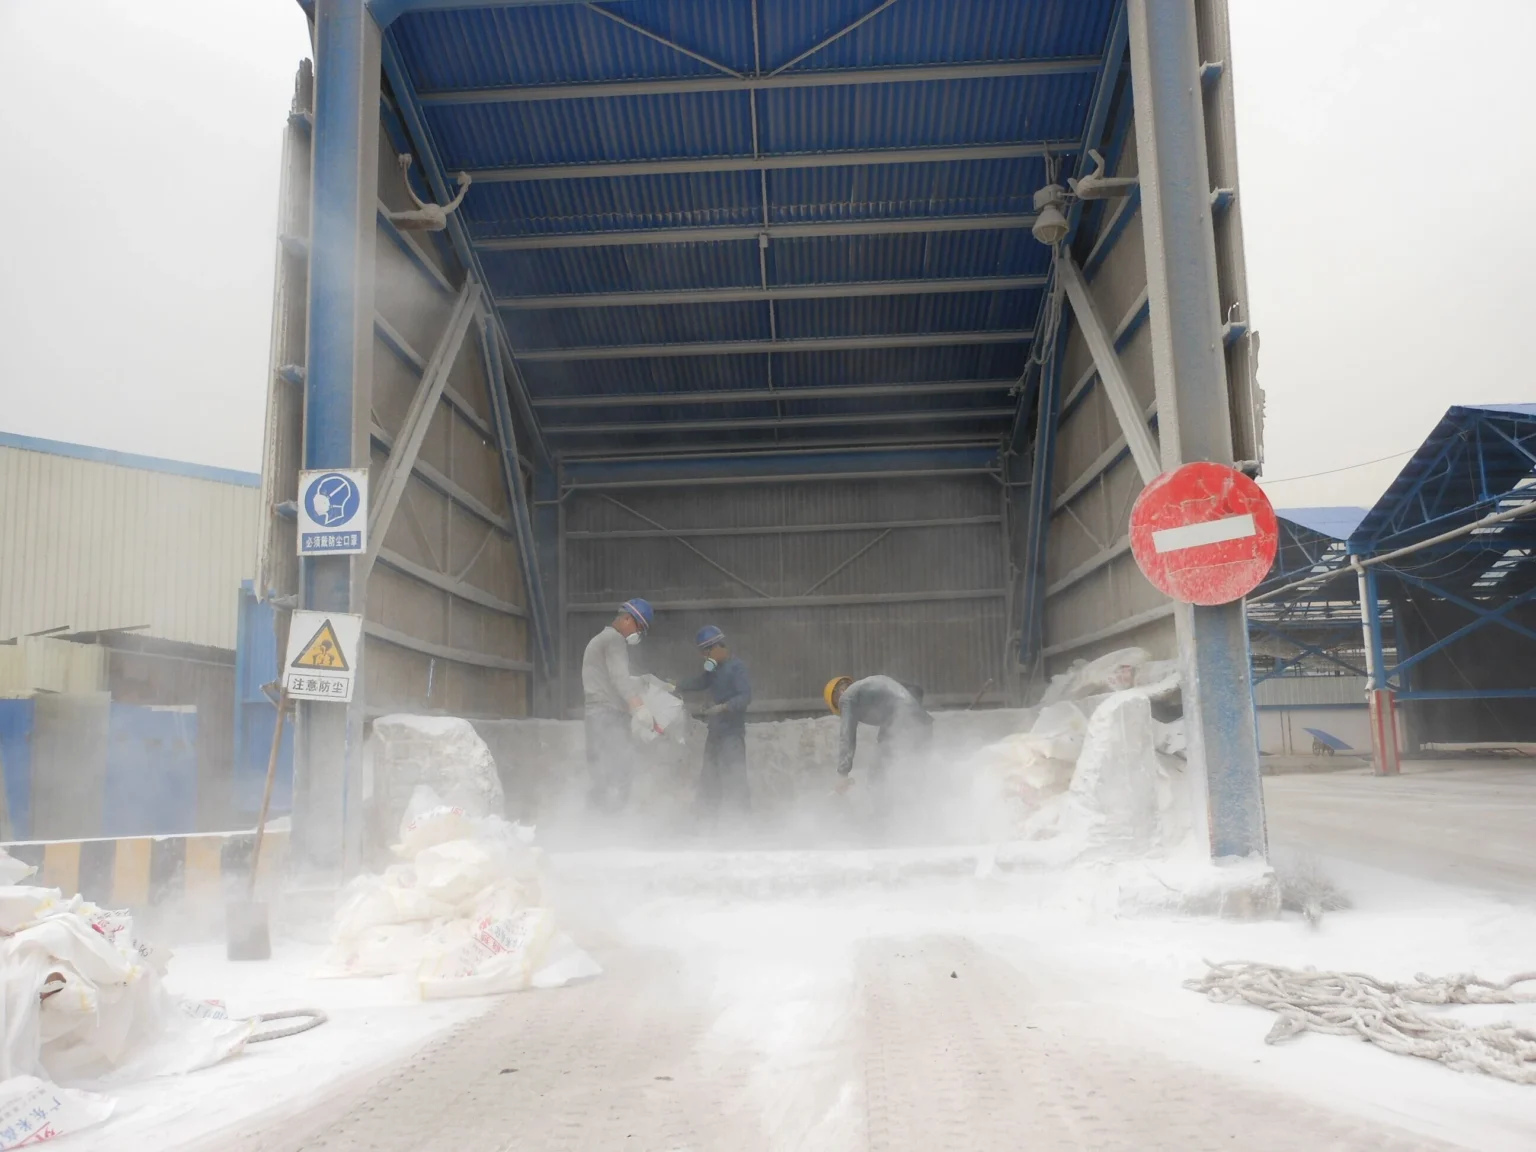
Watch videoThe clouds of dust that escape during the materials handling process pose extreme risks to workers, facilities and environments nearby.
Exposure to such dust can lead to the development of silicosis, lung cancer, and chronic obstructive pulmonary disease for workers.
Dust emissions also threaten equipment reliability and site performance. Fugitive dust settles on machinery, conveyor systems, and electrical infrastructure. Abrasive particles accelerate wear on moving components and contaminate sensitive equipment. This contamination increases maintenance requirements and shortens equipment service life.
Environmental impact also becomes a concern for sites located near coastal areas or sensitive ecosystems. Mineral and chemical dust can settle into nearby water systems, increase turbidity, alter water chemistry, and introduce harmful substances into aquatic habitats. Effective dust suppression at the source protects workers, equipment, and surrounding environments while supporting responsible industrial operation.
Enquire nowGalvanised sheet steel for grain and light materials
Thicker abrasion-resistant steels for rock, ore, and heavy materials
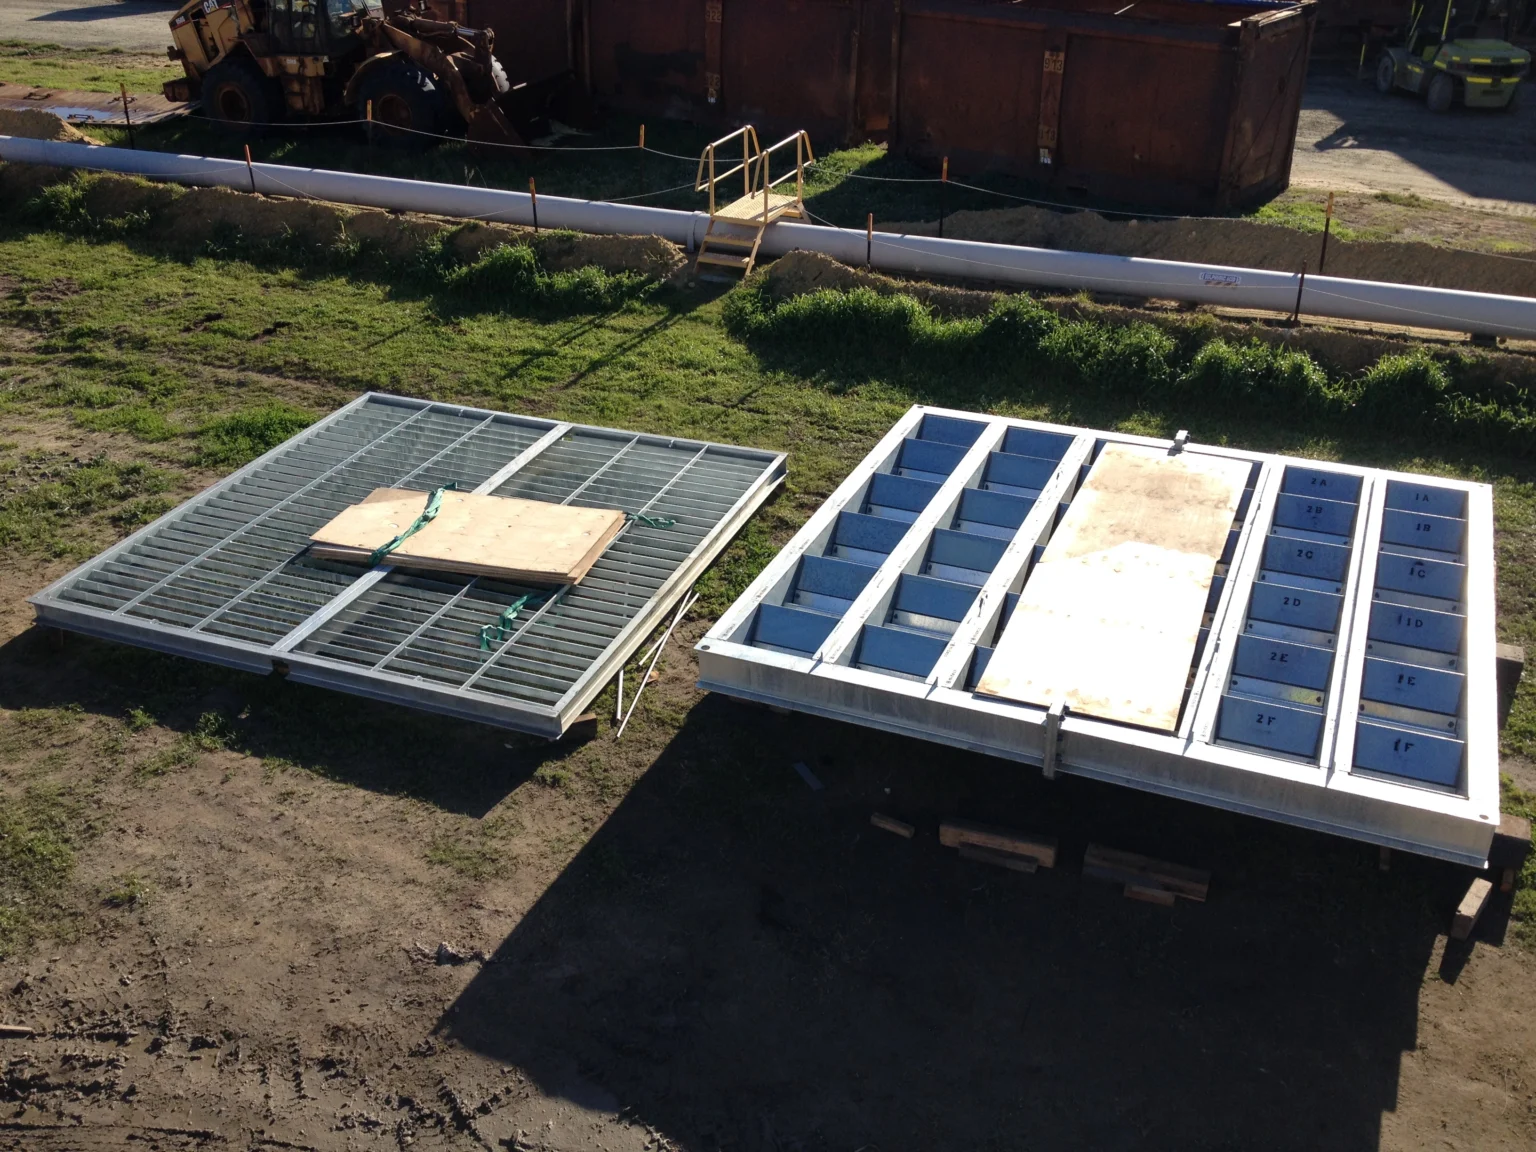
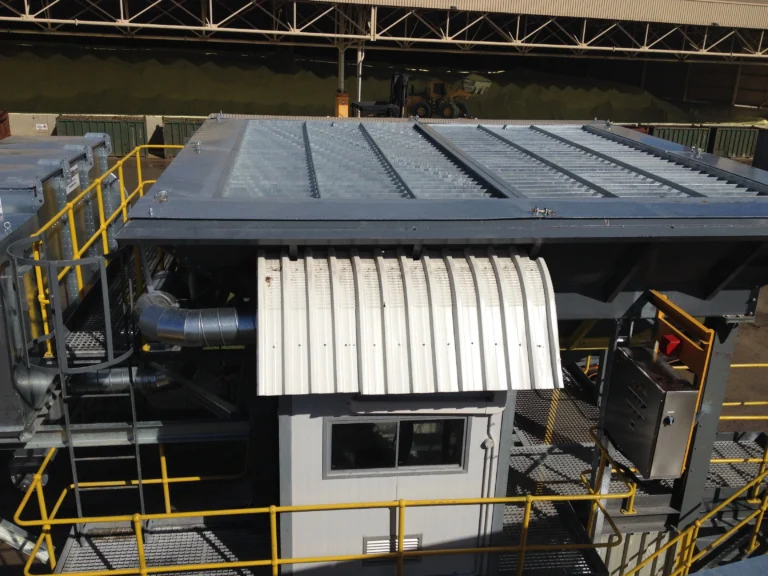
Multiple baffle modules fill the hopper inlet face
Blade assemblies pivot to allow product flow while retaining fine particles
Burnley Baffles protect sites where bulk materials displace large air volumes during transfer.
Common applications include:
They control dust at dump hoppers, receiving pits, and material unloading points where uncontrolled air escape drives particulate release.
During dumping, displaced air inside the hopper accelerates unevenly. High velocity zones carry fine dust and light materials upward through the product stream.
Burnley® Baffles create controlled mechanical resistance across the hopper opening. Multiple tapered modules fill the hopper face. Each module contains pivoting blades that open under the weight of incoming material. As the product flows downward, the blades regulate airflow.
This uniform resistance slows and equalises air speed across the hopper surface. Reduced air velocity prevents particles from lifting into the atmosphere. Fine dust and light materials remain below the blade assembly.
When connected to a negative-pressure system beneath the hopper, displaced air flows downward into a dust collector for full dust capture.
Hopper and receiving pit designs allow displaced air to escape directly through the product stream. High air velocity carries dust into the atmosphere.
Rubber curtains provide limited control and do not equalise airflow across the hopper surface.
Burnley Baffles create structured airflow resistance using gravity-operated baffles. The system controls air speed at the source without electrical power. It reduces emissions mechanically before dust enters the work environment.
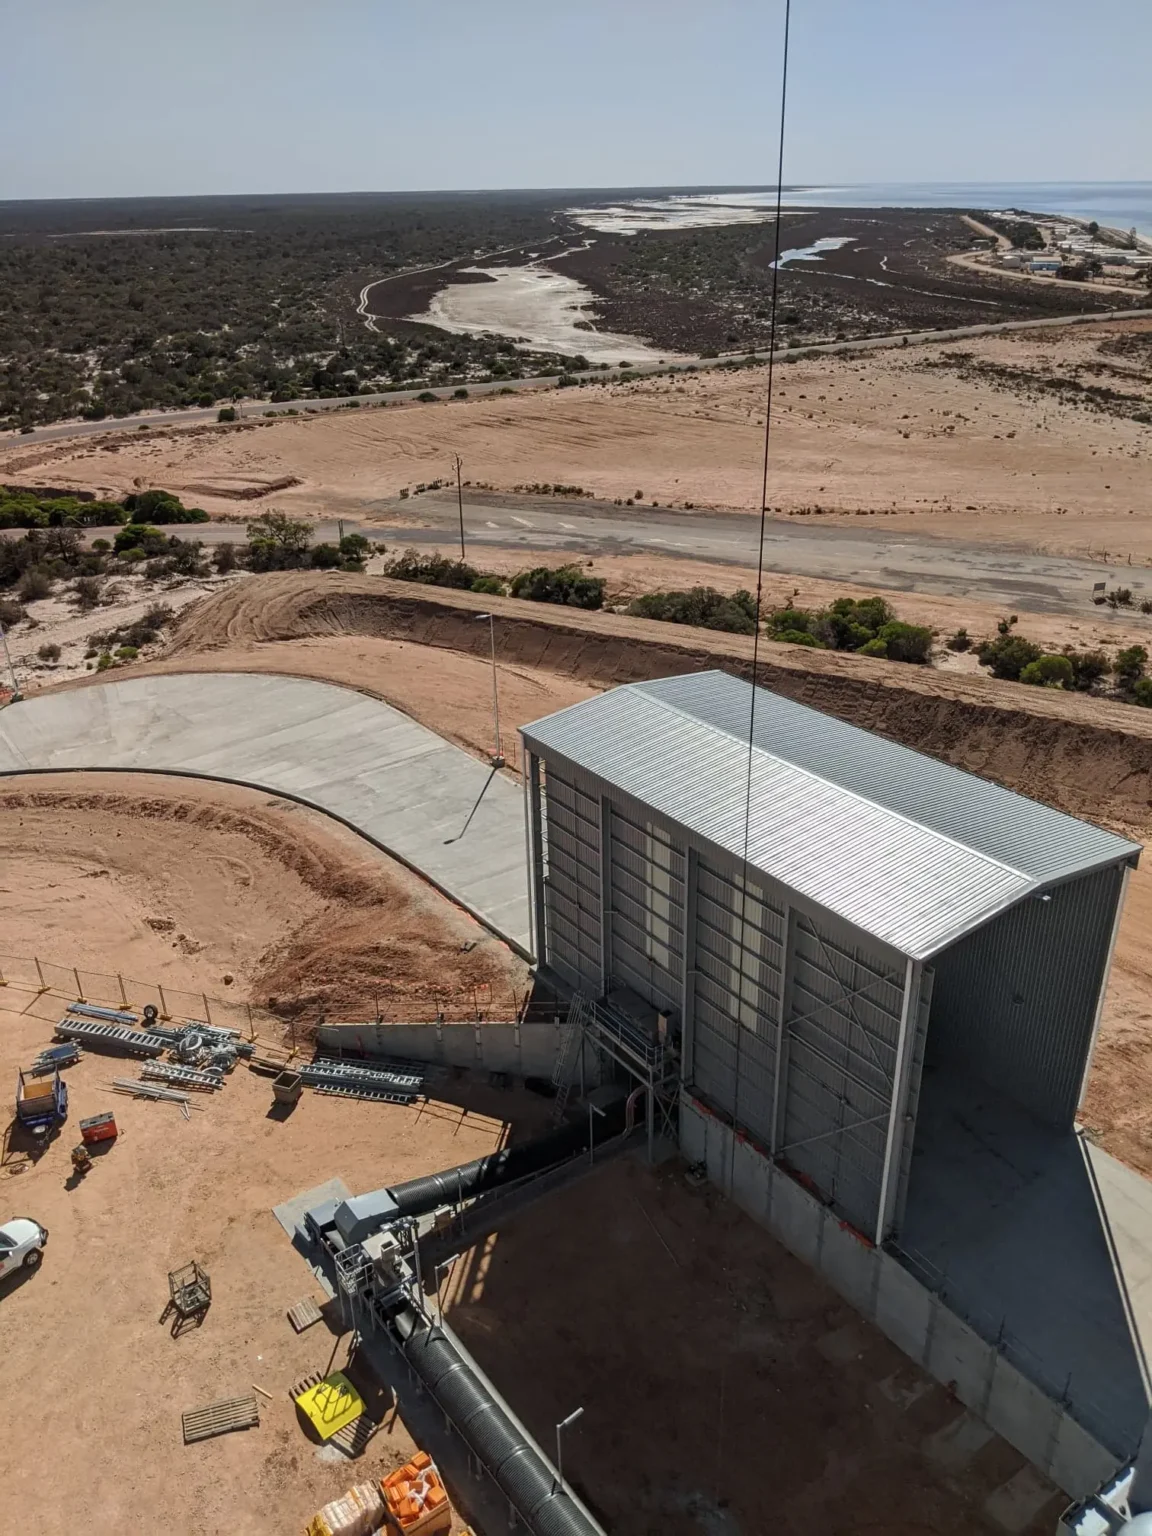
Ahrens required effective dust control at a bulk material handling site where unloading operations generated high airborne particulate emissions. Escaping dust affected visibility, housekeeping standards, and environmental performance.
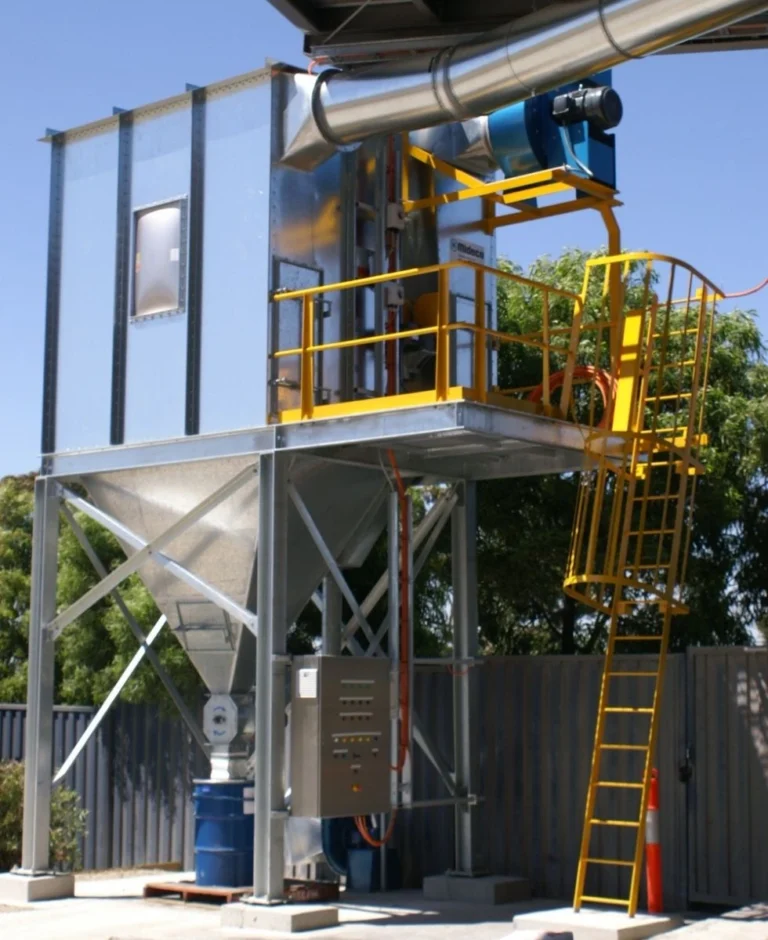
Mideco installed Burnley Baffles across the hopper inlet and integrated an Economy Dust Collector beneath the system. The combined solution reduced visible dust emissions during dumping and improved containment at the transfer point. The site achieved stronger environmental control while retaining valuable material that previously escaped during handling.
See Full Case StudyWhen installed alone, they reduce dust emissions by up to 80%. When combined with a dust collector beneath the hopper, they achieve full dust control.
Yes. Burnley Baffles are not designed to absorb the direct impact of heavy falling material. So a grizzly helps break the fall of materials before they reach the baffles, extending their service life and maintaining form.
Yes. Material options range from galvanised steel for grain to abrasion-resistant steels for rock and ore.
No. The system operates mechanically through gravity.
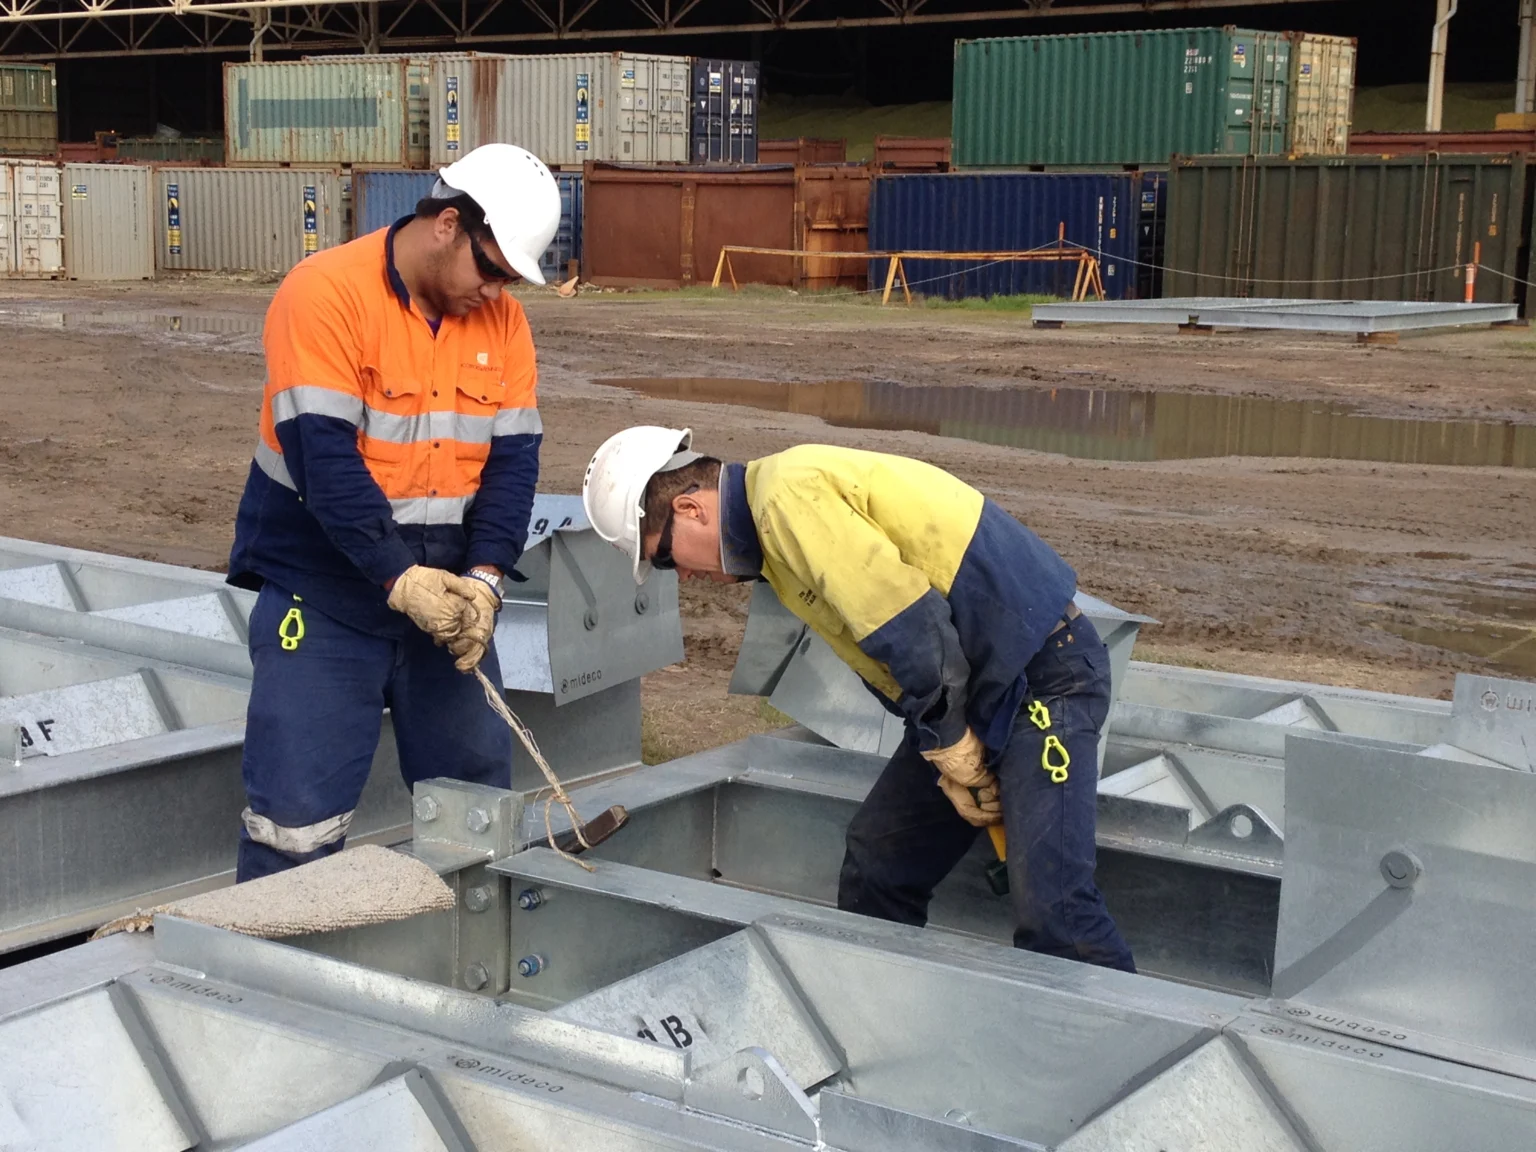
Installation involves placing the units into position according to the general arrangement drawings. Once positioned, the system functions immediately.
Ready to elevate your workplace?
Contact Mideco for innovative dust management solutions.
"*" indicates required fields