Branded products
Dust control solutions
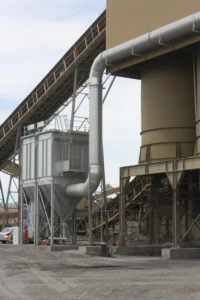
Ahrens is a national full-service construction, engineering and mining services company, delivering a complete range of project services and cost-effective solutions. They had a contract to construct a grain receiving and export facility that required dust management.
Multiple locations required traditional negative pressure dust extractors. However, the grain receival hopper required something more than traditional negative pressure. They also wanted to minimise material handling with regard to dust.
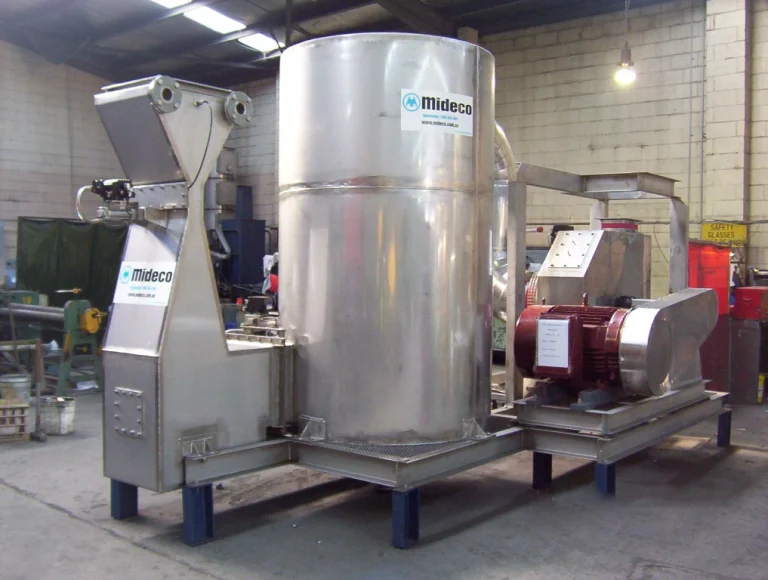
Mideco proposed a solution inclusive of two products, they were Burnley Baffles and Dust Collectors
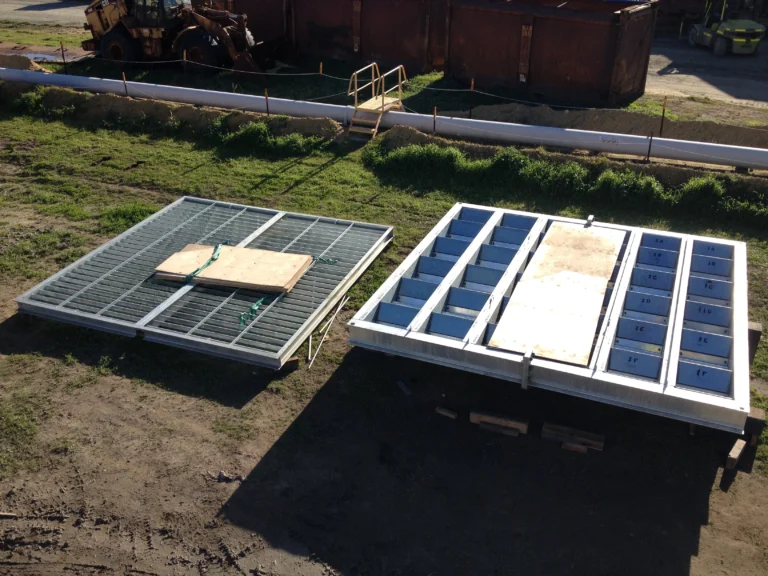
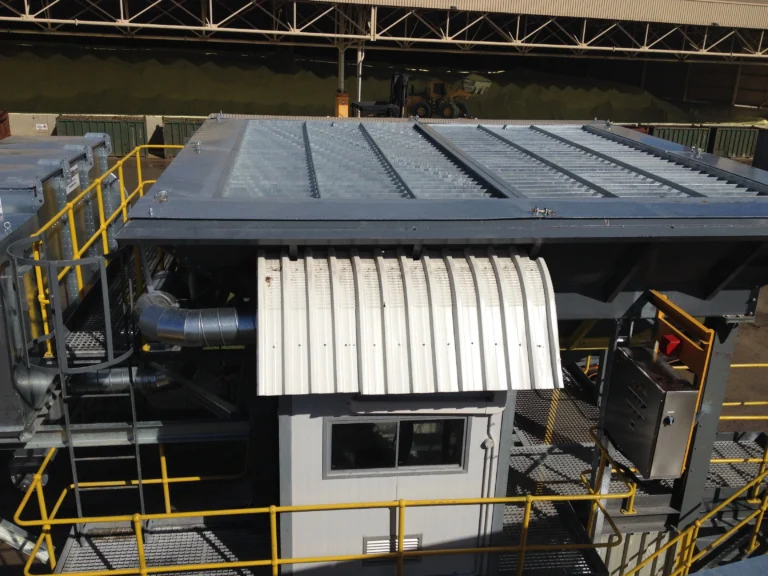
For this application we recommended Mideco Model 1 Burnley® Baffles, 1.6mm thick Galvanised sheet, bolted construction. The hoppers will require support members at the edges and intermittent locations to install the Burnley Baffles.
In applications such as this, the dust is liberated because it is carried by air that is displaced from the hopper when the product is dropped into it. This system operates by enclosing the top of the hopper with Burnley® Baffles. This encapsulates most of the air that would have been displaced. For more information, see the videos on the Burnley Baffles product page.
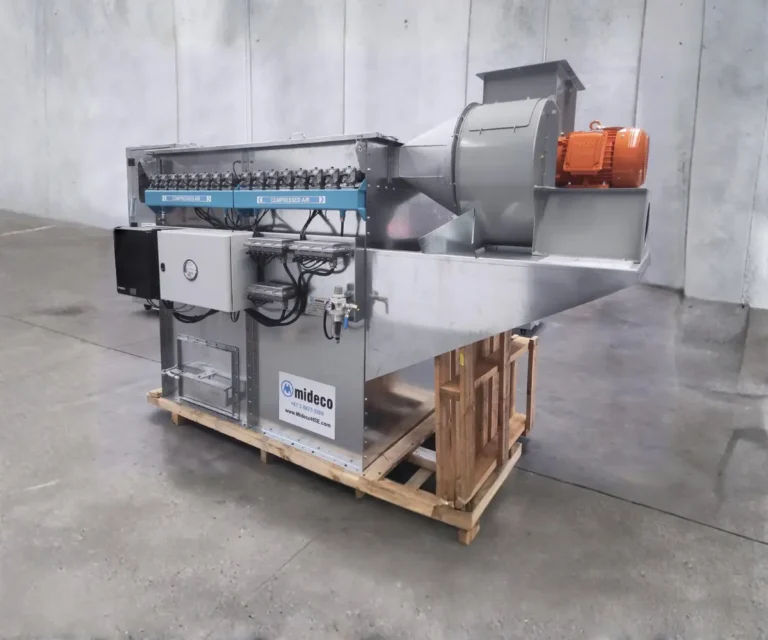
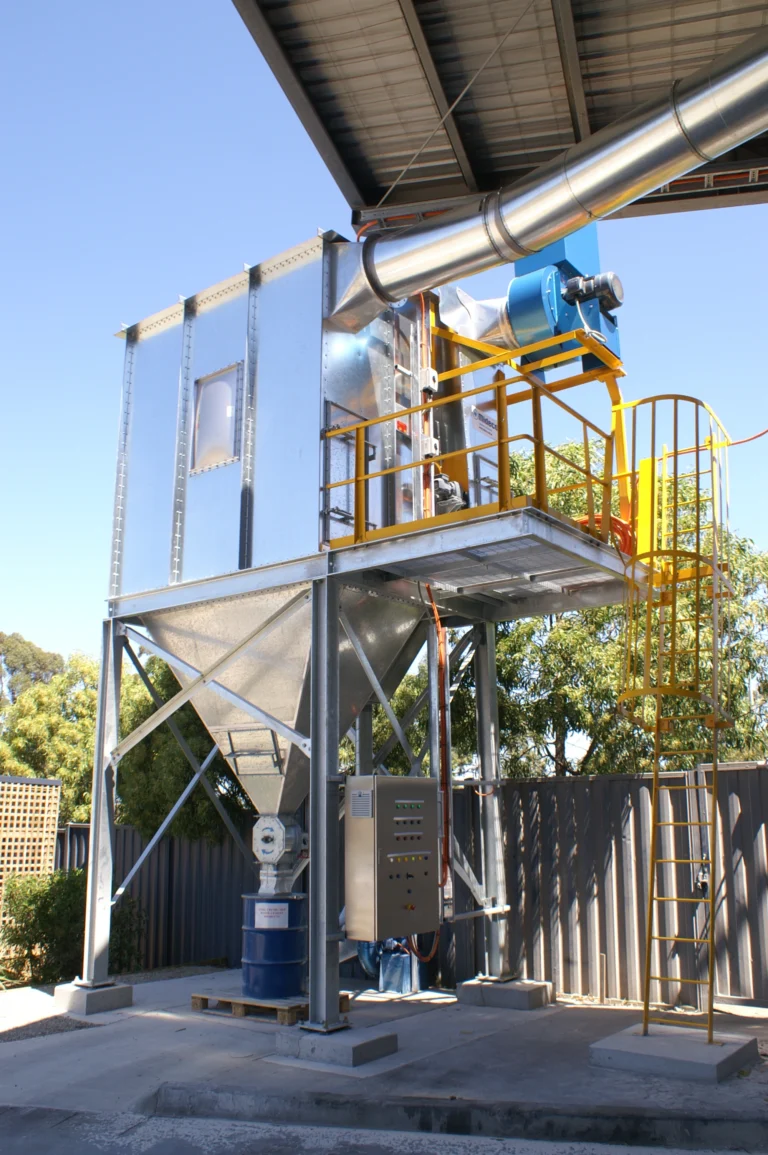
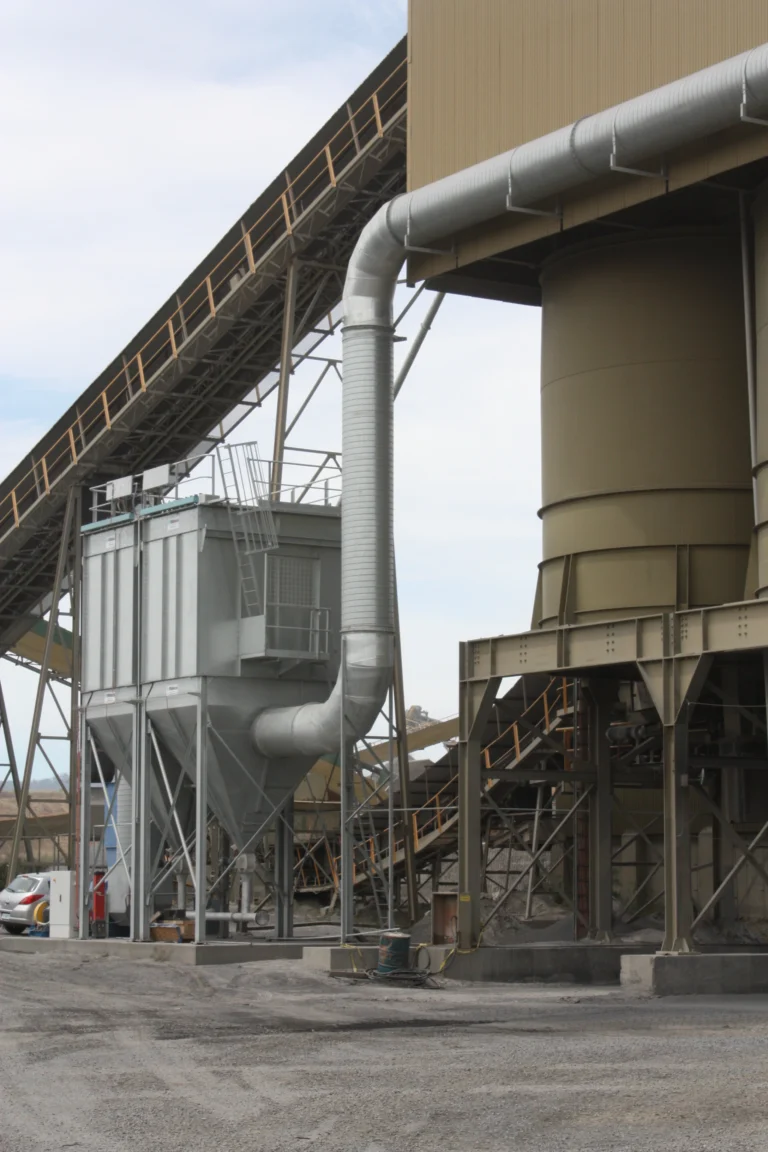
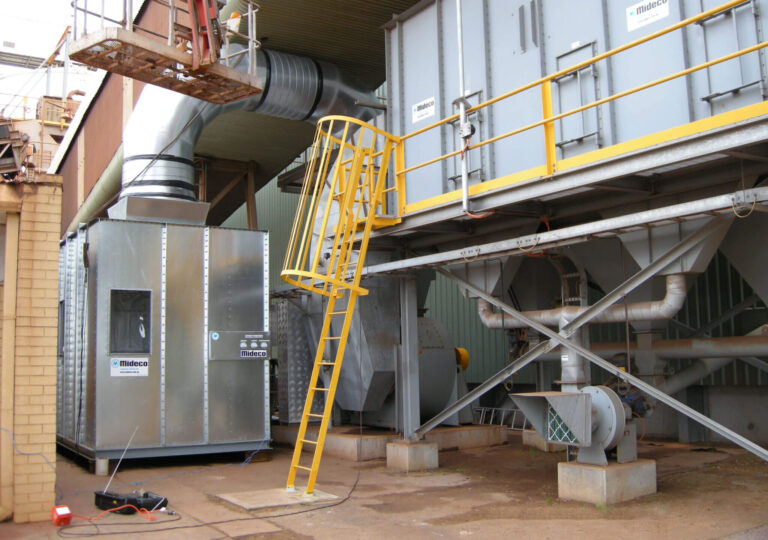
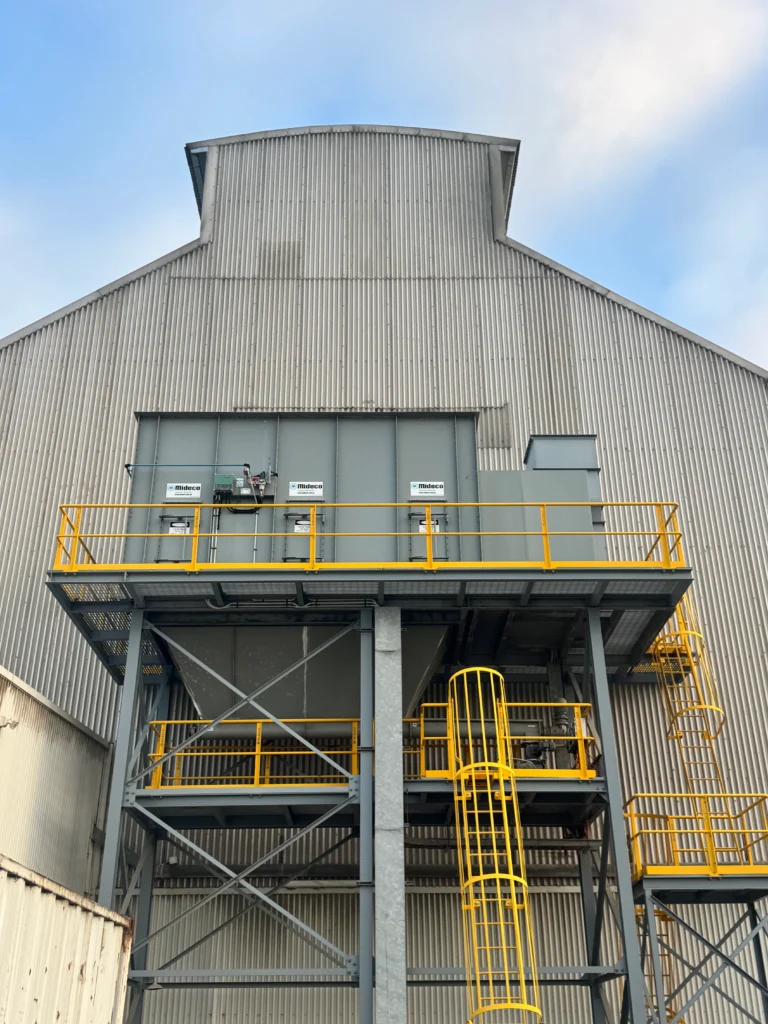
For this application Mideco recommended our range of Economy Jet Pulse Cleaned Dust Collectors which are modular in design, allowing for expansion of the unit to suit varying system requirements.
Each model contains a number of rectangular, envelope style filter bags which are 1.04m long and 0.90m wide. The Mideco Economy Jet Pulse Cleaned range of dust collectors is primarily designed to provide the largest possible cloth area in the smallest case size possible. The design constraints were ease of maintenance inclusive of all the occupational health and safety issues and then being able to use for any labour in the field to perform any given maintenance task.
The Standard Economy Design for this project is inclusive of: