Background
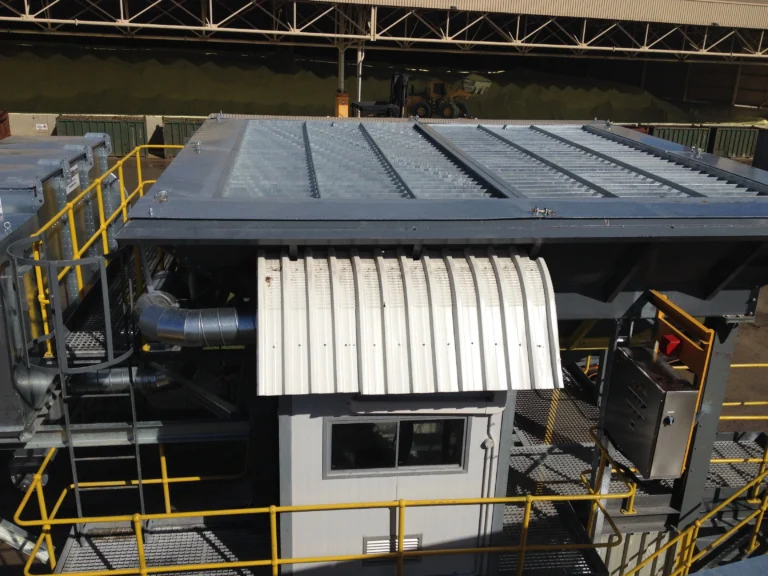
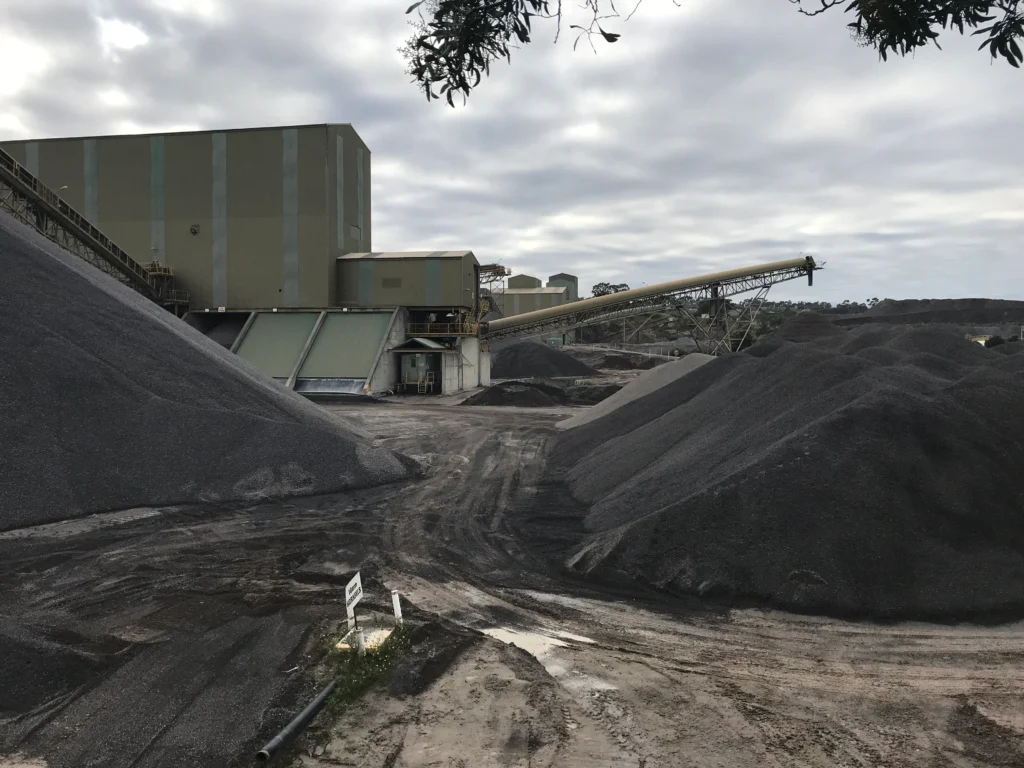
Holcim’s Oaklands Junction Concrete Plant, located north of Melbourne, is one of Victoria’s premier industrial hubs, comprising both a high-production hard rock quarry and a state-of-the-art concrete batching plant.
As a critical supplier for Victoria’s massive infrastructure pipeline, the site operates under intense industrial pressure. The Oaklands Junction Quarry is a high-output environment where hard rock extraction and processing generate significant quantities of respirable silica.
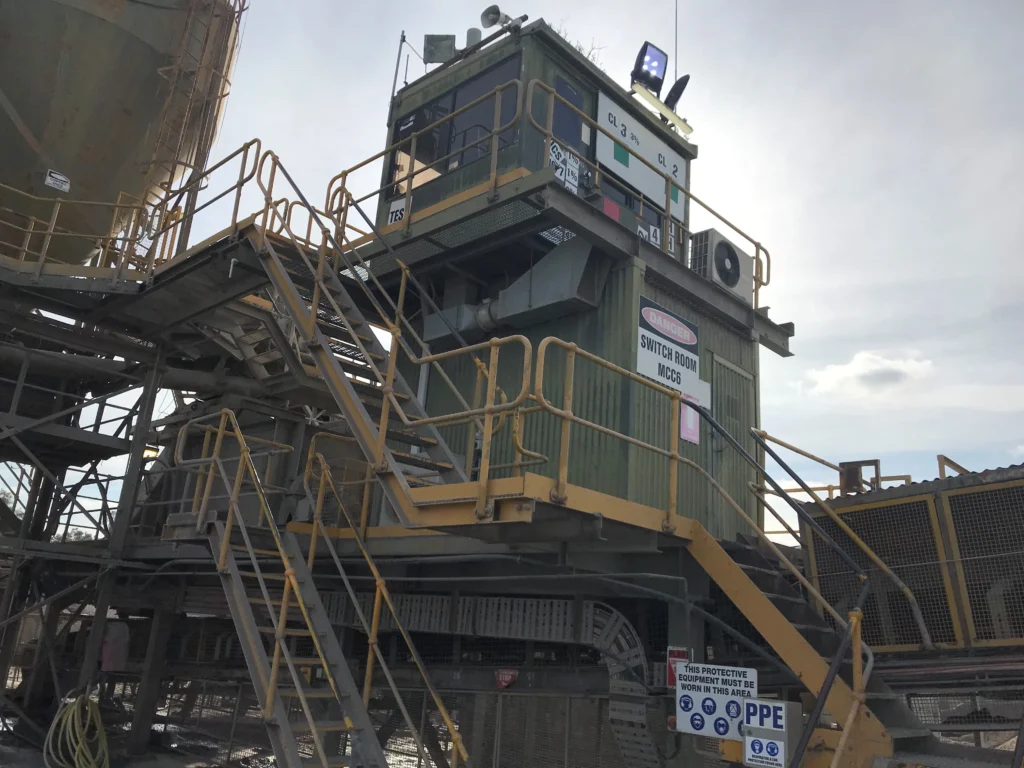
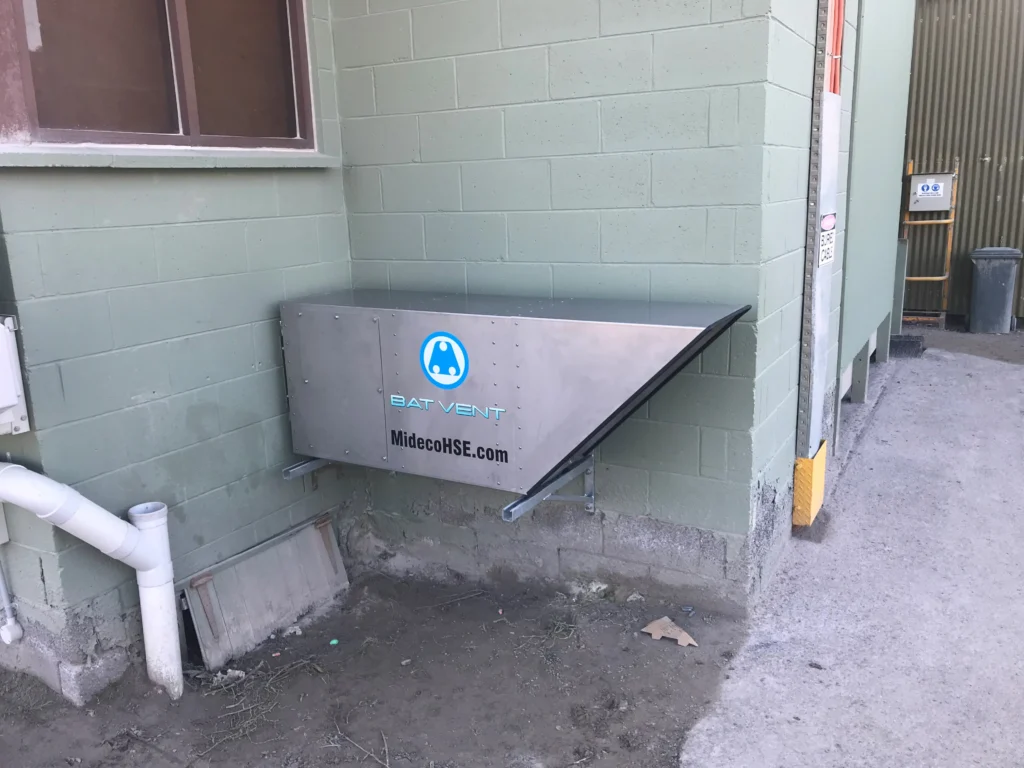
Holcim’s commitment to safety and innovation at this site made them the ideal partner for the Bat Vent’s development. They required a solution that could protect personnel in site offices and control rooms without compromising the high-velocity operational needs of the site. It was here, amidst the heavy machinery and constant movement of Melbourne’s northern infrastructure space, that the Bat Vent was created.
Recognizing the Problem and Gap
The Bat Vent was born from a commitment to bridge a critical gap in industrial safety of protecting workers from the threat of indirect dust exposure in site offices and control rooms. Faced with a lack of specific Australian standards for these environments, the design was engineered to meet the world’s most stringent criteria, specifically the US NIOSH recommendations and Queensland’s Recognised Standard 20 (RS20).
This approach ensured the system was not only technically superior but also legally defensible in the face of rising silica-related health challenges. By adopting these standards, Mideco transitioned from general observations to a pointy-end engineering solution. Ultimately, the Bat Vent stands as a proactive response to the need for a rigorous safety benchmark in the fight against respirable dust.
Initial Components
The technical evolution of the Bat Vent shifted the focus from a basic fan to a sophisticated pressure-management system. By integrating a VSD (Variable Speed Drive) with a pressure-controlled feedback loop, the system maintains a constant positive pressure barrier against hazardous dust. To ensure the system remains stable and defensible, the following components were integrated:
- Pressure-Controlled VSD: Automatically adjusts fan speed to maintain the specific pressure required to keep silica dust out of the clean zone.
- Damping: Prevents the fan from over-revving when a door is momentarily opened, extending motor life and maintaining consistent air quality.
- 4-20mA Signal Output: Enables continuous data logging of room pressure for compliance and auditing.
- Filter Monitoring: A dedicated signal for cartridge changes ensures the system never operates at sub-optimal levels.
Prototyping
The next stage involved moving from theoretical standards to a prototype phase. Rather than launching a finished product, our team developed a Room Pressuriser, a programmable unit designed to be a universal solution for hazardous environments.
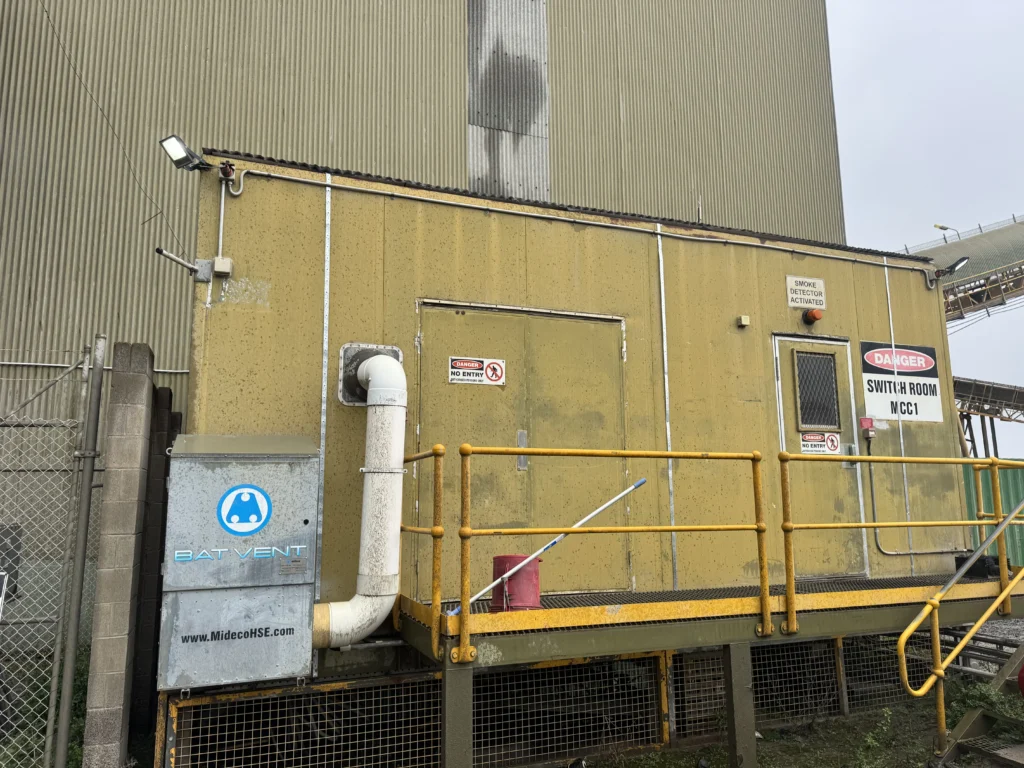
Mideco supplied the first unit to Holcim Oaklands Junction as a prototype, which allowed their own site teams to perform the installation and provide the raw, honest feedback needed to refine the design for rugged field use. To ensure the system was intelligent enough to meet stringent legal standards, we invested heavily in custom programming. Furthermore, the team addressed the variable of how the system would handle real-world site offices, which are rarely airtight, to maintain a safety barrier even within imperfect structures.
Engineering Breakthroughs
The team moved to creating a data-driven defense system based on Recognised Standard 20 (RS20) benchmarks:
- Utilizing H13 cartridges as the primary barrier with a mandatory annual replacement policy.
- While the system targets a certain level of positive pressure, it includes a critical safety floor so when pressure drops to a limit, the system triggers an immediate operator warning.
- We ditched old-fashioned mechanical gates which are prone to leaks for a computer-controlled fan that reacts instantly to pressure changes.
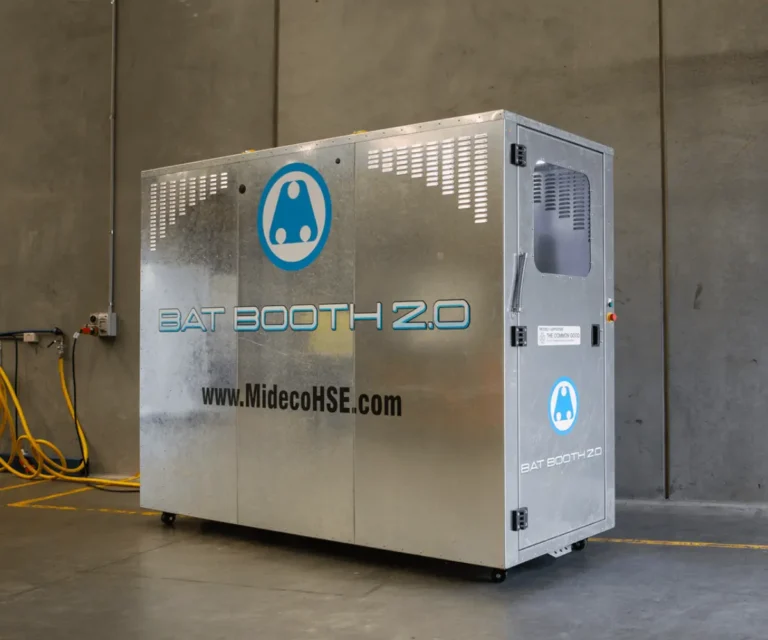
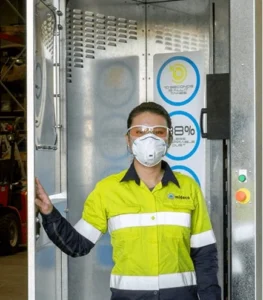
- Recognizing that dust is carried on clothes, Mideco added a pre-filter stage and recommended the system be used alongside the Bat Booth® personnel de-dusting systems.
Programming Logic
The next hurdle was translating complex safety ideas into sophisticated software logic. While waiting for final components, we spent weeks testing the fan’s performance curve to ensure absolute stability. This temporary setup also enabled the team to perform noise testing and verify that the system remained quiet enough for a productive office or control room environment. Ultimately, Mideco made a significant investment in custom programming to ensure the system could intelligently handle the unpredictable pressure fluctuations common in real-world site cabins.
The Vote of Confidence
The six-unit order marked the transition from prototype to mission-critical safety standard. This commitment highlighted a profound level of trust in Mideco’s engineering. The urgency of target date underscored that the Bat Vent was an essential infrastructure requirement. Despite supply chain complexities, the Holcim’s commitment on this timeframe proved the high value placed on protecting their most valuable asset, their people.
Testing
The team conducted stress tests by cutting a hole in our own office lunchroom wall to ensure the system could handle real-world variables. By testing in a high-traffic area where people constantly come and go, we simulated conditions far more arduous than those found in a standard control room. We found that while the unit could easily hit the target pressure in a leaky room, it only needed a small fraction of its power to maintain that safety barrier once the room was properly sealed.
We also addressed the noise of high-velocity air by integrating internal soundproofing. This brought the noise down to a comfortable level, ensuring the system protects the team without disrupting their work.
Standardisation
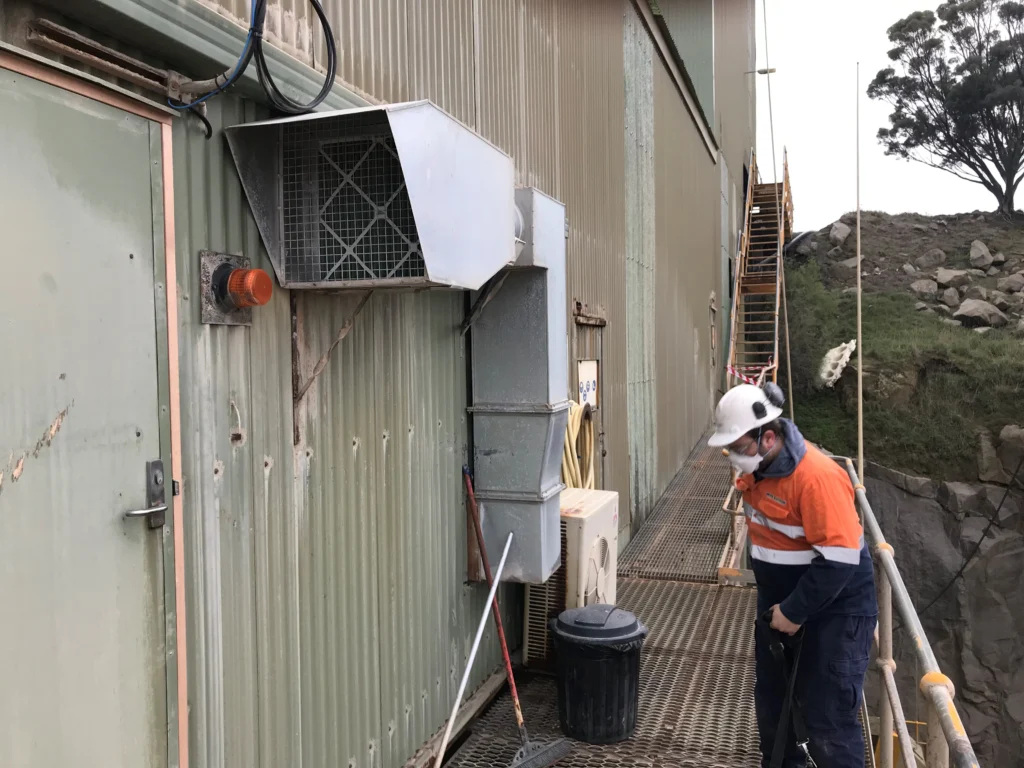
The final design phase focused on transforming the unit into a true plug-and-play product that site teams could deploy with ease. The team developed an offset spigot for maximum flexibility, allowing the unit to be installed either parallel or at 90 degrees to any wall surface. To accommodate the variety of structures found on-site, we provided a kit that utilizes specialized clamping rings and a telescopic duct system that ensures a perfect, airtight fit regardless of the wall thickness. Mideco also included high-quality seals to protect wall cavities from moisture and mesh covers for a presentable finish within the office environment. Finally, the entire system was designed to run on standard single-phase power, ensuring it remains accessible for any site office without the need for specialized electrical infrastructure.
Precision Machining
Then, the Bat Vent saw a strategic shift toward precision machining, where basic steel fabrications were replaced with a refined, high-tolerance spigot and grate system. These components are designed to slip into the ducting perfectly, ensuring a repeatable, airtight seal that maintains room integrity. We also listened to feedback about the work environment and built soundproofing right into the assembly to keep the noise at a minimum. We even added simple cable clips and routing options to simplify the final installation process.
This design revision culminated to a revolutionary leap in efficiency that achieved greater performance. By optimizing the internal layout, we managed to double the filtration area for dust capture without making the unit any larger, making the Bat Vent even easier to install in the tight, space-constrained environments typical of industrial site offices.
Client Feedback & The Future of Bat Vent
The ultimate validation of the design process came from the field. Following the initial rollout, the feedback from Holcim team confirmed that the transition from a Room Pressuriser to a refined safety system was a success. They highlight:
“The updated unit [Bat Vent 1.0] appears to be working a lot better than the original [prototype].”
This successful collaboration paved the way for the Bat Vent 1.0 to become a permanent fixture in site safety infrastructure. In the years following its 2021 development, Mideco has received subsequent orders from Holcim, cementing the system’s reputation as a reliable, essential tool for silica dust control.
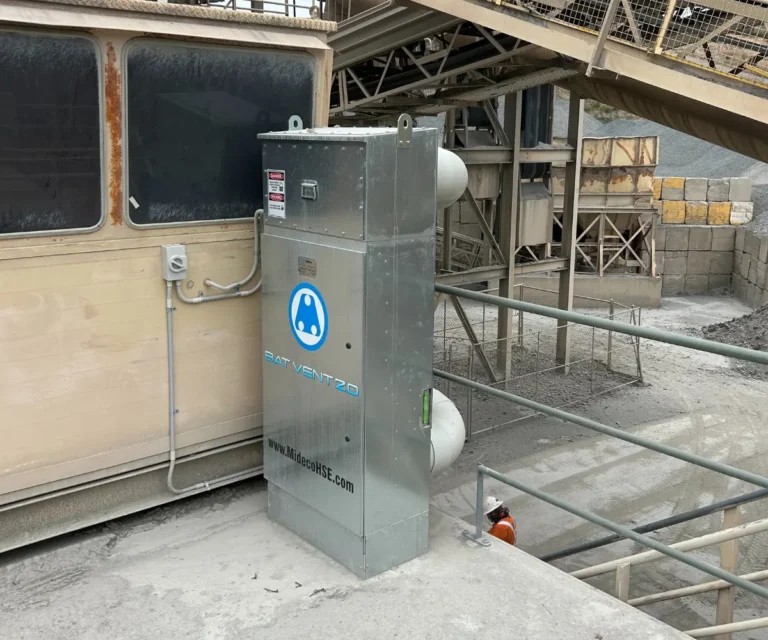
In 2023, redesigned with a sleek new body, the Bat Vent 2.0 offers faster installation, better site integration, and significantly improved airflow. Ideal for both retrofit and new builds, it delivers outstanding protection against airborne dust. This next-generation system reflects Mideco’s commitment to innovation and worker safety.
 AU
 US